




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
CNC Machining vs. Additive Manufacturing: Selecting the Ideal Method for Low-Volume Spare Parts
Introduction: The Evolving Landscape of Spare Parts Manufacturing
As industrial maintenance and custom equipment manufacturing demand faster turnaround times, choosing between additive manufacturing (3D printing) and precision CNC machining for low-volume replacement components has become a pivotal technical decision. While 3D printing excels in creating intricate, low-stress structures, subtractive CNC machining remains indispensable for critical hardware operating under demanding mechanical loads, high thermal stresses, and tight fitting requirements.
Key Technical Drivers & Decision Criteria
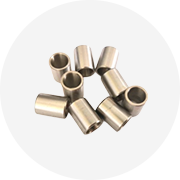
- Tolerances and Geometric Precision: High-precision components such as tapered lock pins, locating studs, and ground dowel pins require fit classes like h6, h7, or m6 with tolerances reaching ±0.03 mm. CNC milling, turning, and cylindrical grinding achieve these specifications consistently, whereas unmachined 3D-printed parts typically fall short without extensive secondary finishing operations.
- Metallurgical Density and Structural Isotropy: Machined parts made from wrought bar stock—including 304/316 stainless steel, 4140 alloy steel, C45 carbon steel, and brass—retain uniform mechanical strength across all axes. In contrast, metal 3D printing can introduce anisotropic layer weaknesses and micro-voids, increasing vulnerability under high shear loads.
- Hardness and Surface Integrity: Components subject to continuous friction or impact rely on heat treatment techniques such as quenching, tempering, and induction hardening to achieve HRC 45–62. Machined hardware easily accommodates these thermal treatments to provide long-lasting wear resistance.
- Scalable Production Flexibility: Subtractive processes support low-volume prototyping starting from 1 to 10 sample pieces, smoothly scaling to batch production of 50 to 500 units or 1,000+ mass production volumes with reliable lead times of 7 to 15 days.
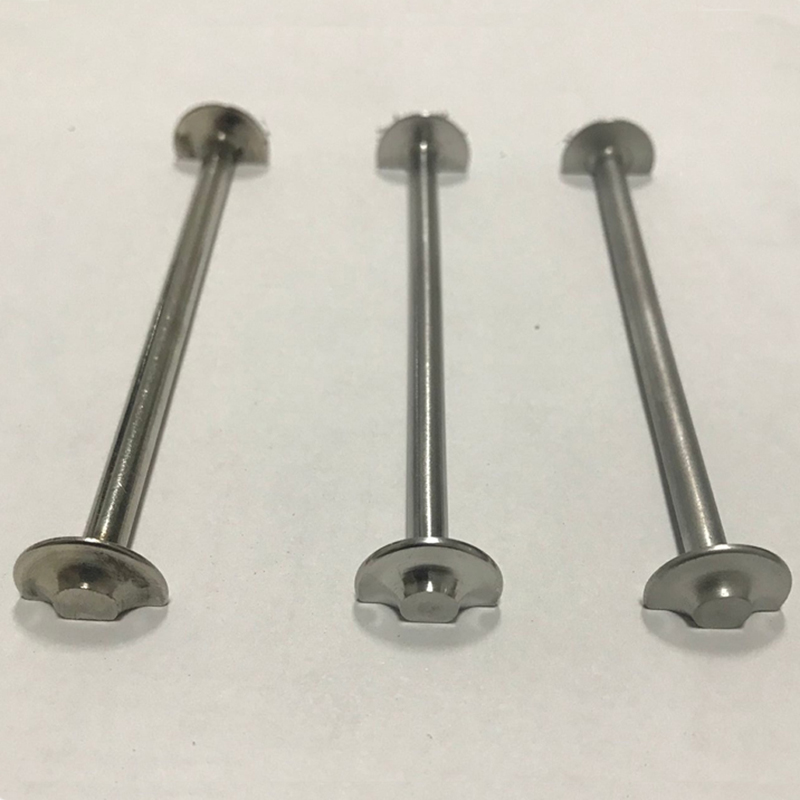
Engineering Principles: Load-Bearing Requirements vs. Geometric Flexibility
Determining whether a part can be 3D printed or must be CNC machined depends heavily on its functional role. Additive manufacturing offers significant advantages for lightweight enclosures, internal fluid distribution channels, and non-load-bearing brackets. However, when a component acts as a mechanical fail-safe—such as a shear pin in drive systems—predictable material failure limits are essential. CNC machining ensures homogeneous density and consistent shear behavior that additive processes struggle to replicate reliably.
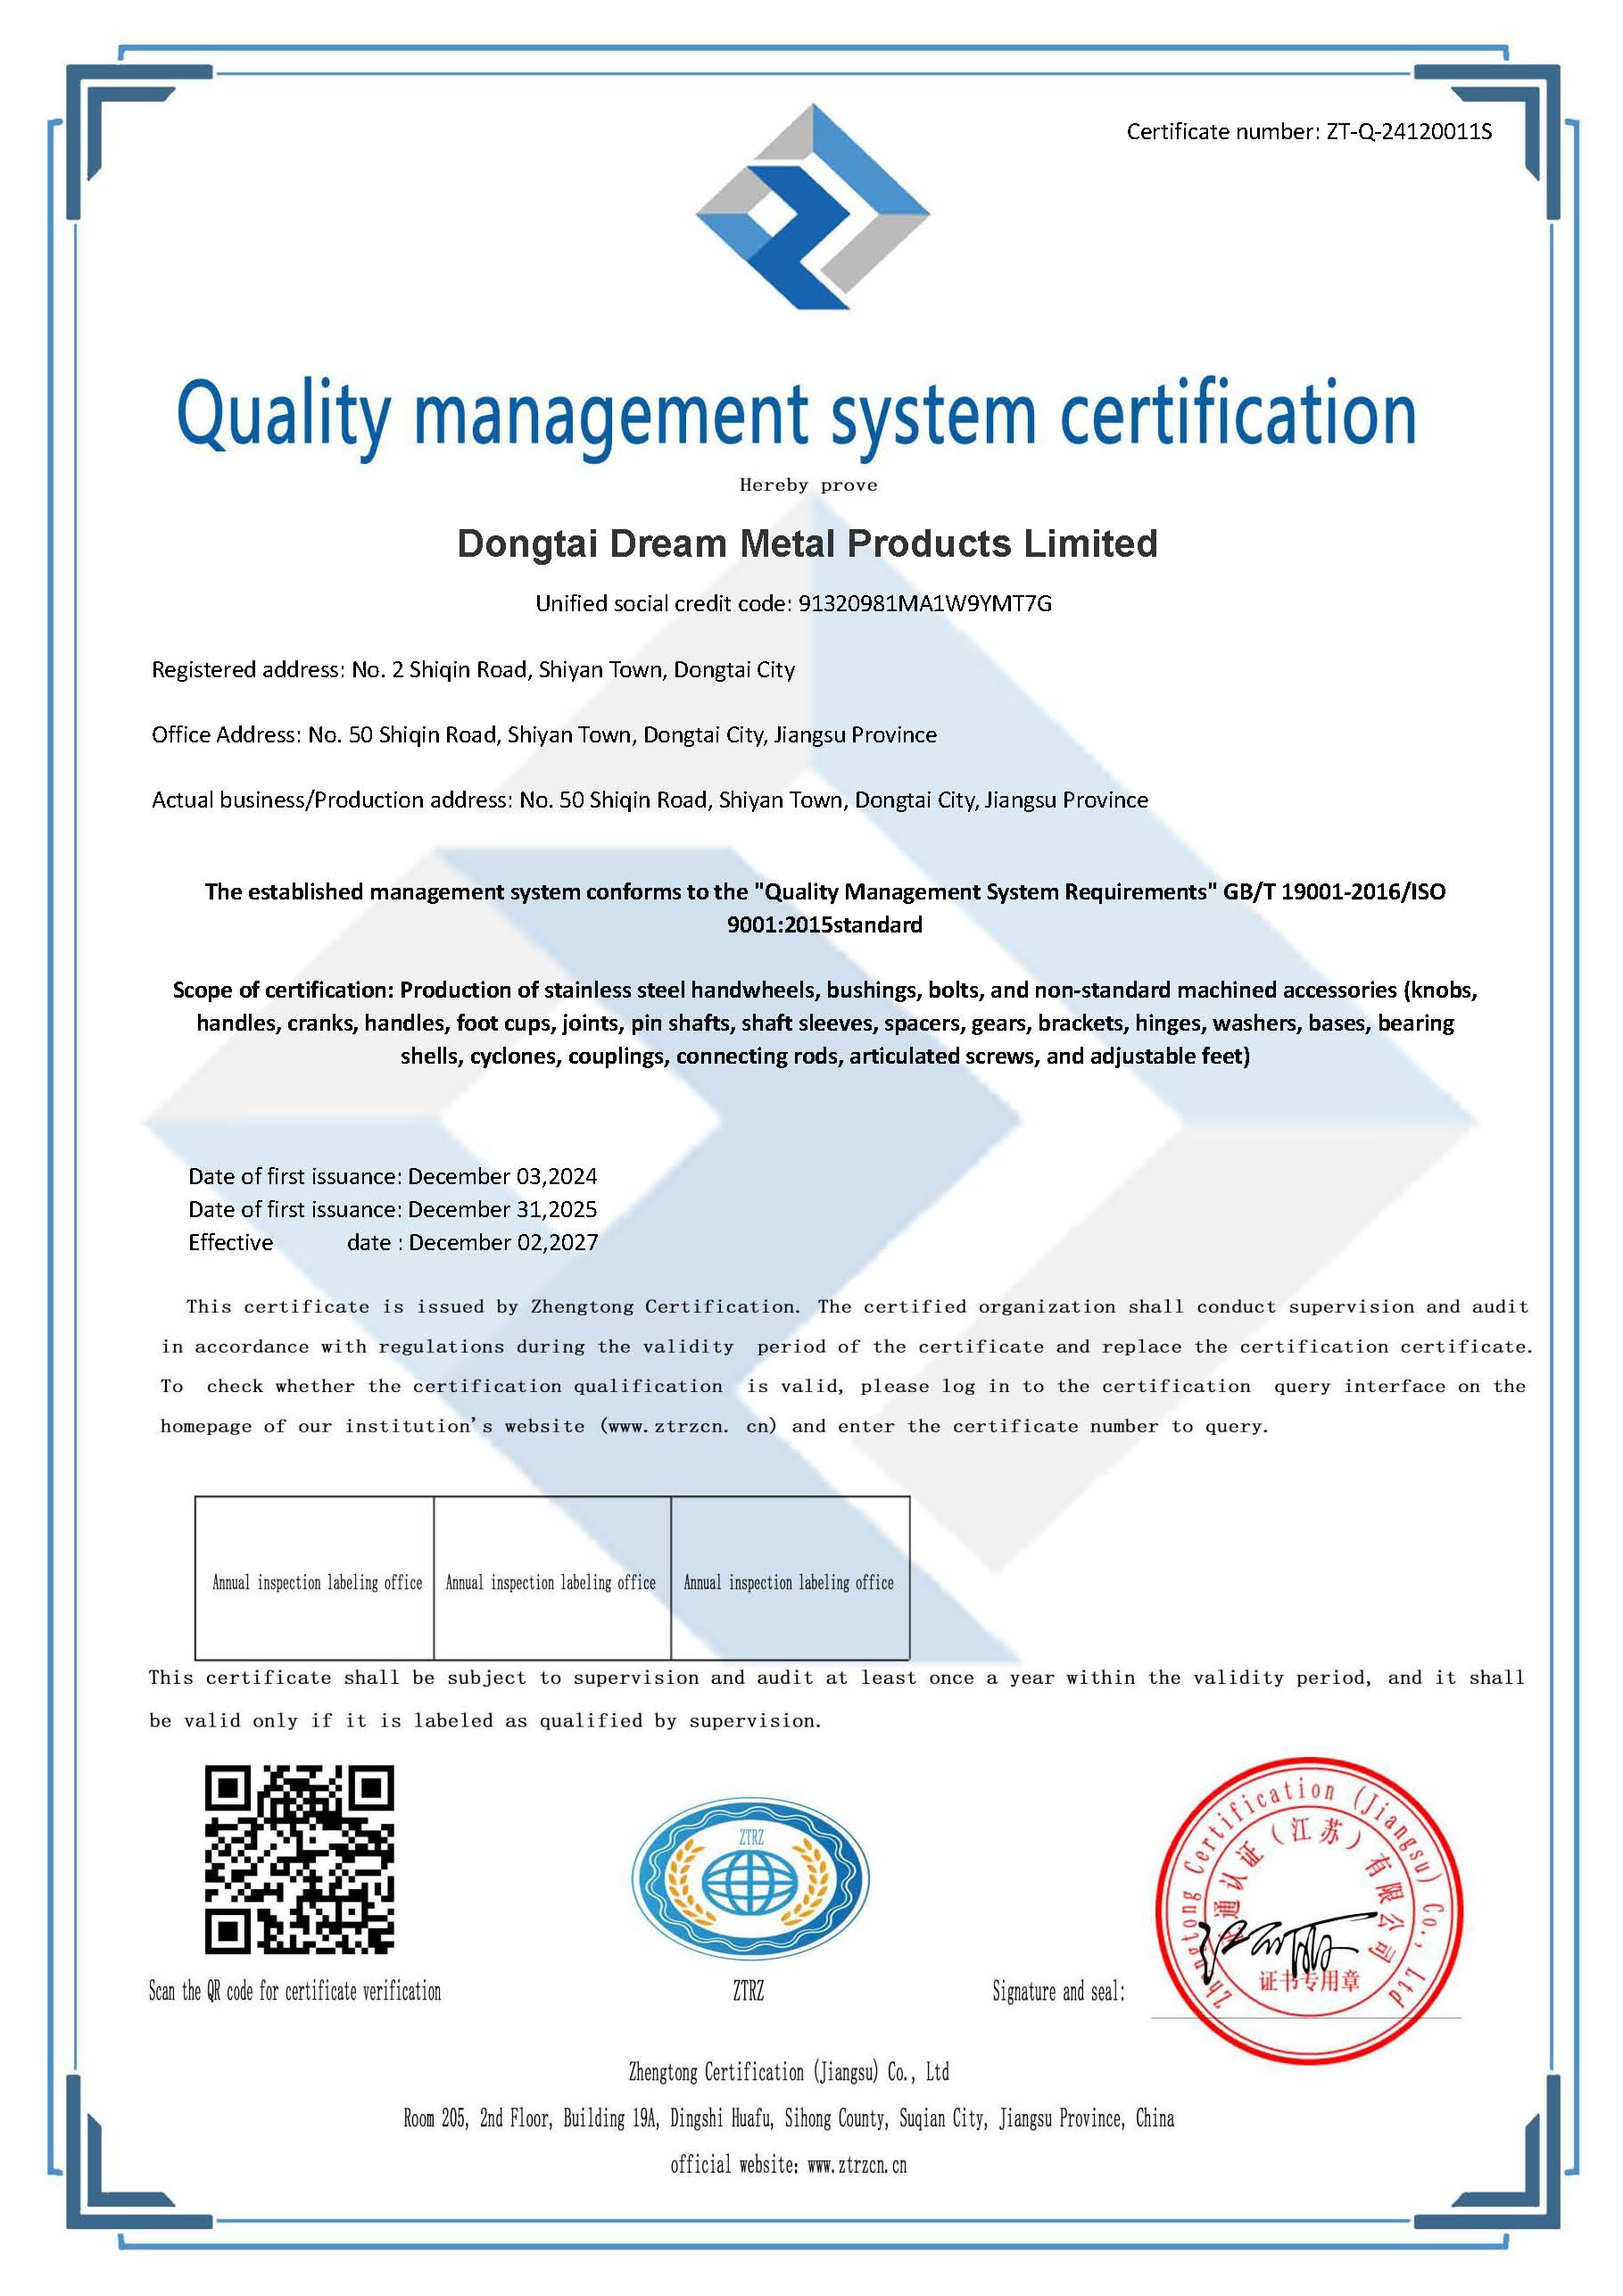
Furthermore, surface treatment compatibility plays a crucial role. CNC turned and ground components feature fine surface finishes that readily accept passivation, electropolishing, black oxide coating, or zinc plating. Quality assurance protocols, aligned with ISO 9001 standards (Certificate ZT-Q-24120011S), implement multi-stage inspections (up to 23 steps) to restrict dimensional variation to within ±0.03 mm and maintain defect rates under 0.3%. Field implementations in European machinery manufacturing and North American valve production demonstrate that precision-machined alignment components prevent severe equipment misalignment and costly operational disruptions.
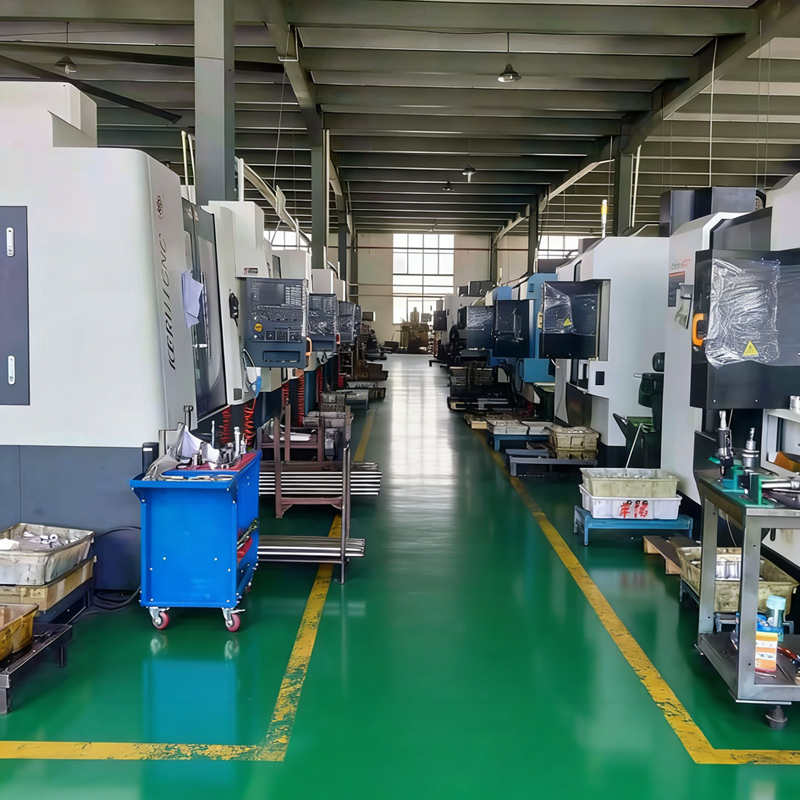
Performance & Parameter Comparison Table
Below is a comparative breakdown of key operational characteristics between Additive Manufacturing and Precision CNC Machining for short-run component manufacturing:
| Operational Parameter | Additive Manufacturing (3D Printing) | Precision CNC Machining |
|---|---|---|
| Dimensional Tolerance Limits | ±0.1 mm to ±0.3 mm (As-printed) | ±0.03 mm to ±0.05 mm (Fits h6/h7/m6) |
| Achievable Hardness Levels | Requires post-process heat treating | HRC 45–62 (Quenched, Carburized, Hardened) |
| Material Versatility | Selected printable metal powders & polymers | 304/316 SS, 4140 Alloy, C45 Steel, Brass |
| Surface Texture & Finishing | Noticeable layer boundaries; requires finishing | Precision ground, polished, passivated, plated |
| Low-Volume Prototyping Flexibility | Excellent for complex non-load geometries | Excellent for functional samples (1–10 pcs) & batches |
| Mechanical Behavior | Anisotropic across print layers | Fully isotropic structural integrity |
Frequently Asked Questions
When is CNC machining preferred over 3D printing for replacement components?
CNC machining is recommended when parts must meet strict fit tolerances (±0.03 mm), specific surface hardness ranges (HRC 45–62), ground finishes, or demanding dynamic loads in industrial equipment, valves, and automation systems.
Which technical standards apply to precision dowel and alignment pins?
Precision locating pins commonly conform to ISO 2339, DIN 1, and DIN 258 specifications, using h6, h7, or m6 fit tolerances and standardized 1:50 tapers for positive mechanical locking and precise repeatability.
Can custom machined spare parts be produced in small prototype quantities?
Yes, versatile OEM/ODM manufacturing setups easily accommodate prototype runs from 1 to 10 units, small production batches of 50 to 500 units, and full production volumes over 1,000 pieces with typical lead times of 7 to 15 days.
Conclusion & Strategic Guidance
While 3D printing is an excellent tool for conceptual prototypes and complex, non-critical housings, subtractive CNC machining remains the gold standard for functional mechanical components that demand tight positioning, high torque retention, wear-resistant surface hardness, and corrosion immunity. Partnering with experienced OEM/ODM suppliers using advanced CNC equipment ensures precise part interchangeability and extended service life. For engineering inquiries or custom manufacturing support, contact our team at 86-15868979792.
Company Overview
Zhejiang Dream Industry Limited is a dedicated provider of precision hardware design, CNC turning and milling, and custom mechanical component fabrication. Founded in 2008, the company operates a modern 2,500-square-meter facility with 34 skilled staff members, including seasoned engineering specialists and quality control inspectors. Equipped with automated CNC turning centers, high-precision lathes, and laser welding systems, the plant delivers an annual capacity exceeding 3 million precision parts. Certified under ISO 9001 (Certificate ZT-Q-24120011S), the enterprise delivers customized OEM/ODM hardware solutions to global clients in the automation, industrial valve, marine engineering, and food machinery sectors across North America, Europe, South America, and Southeast Asia.
REPORT