




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
Essential Wall and Roof Specifications for High-Performance Detachable Container Houses
When selecting a detachable container house, the durability, energy efficiency, and structural safety depend fundamentally on the engineering of its wall and roof systems. Core insulation materials, panel thickness, anti-corrosion treatments, and sealing mechanisms dictate how well a modular unit withstands environmental stress across temperature extremes from -40°C to +50°C. Utilizing 70–100mm closed-cell polyurethane (PU) or rock wool sandwich panels alongside hot-dip galvanized steel framing yields superior thermal insulation, IP65 moisture protection, and wind resistance rated up to Grade 10–12.
Key Highlights & Engineering Takeaways
- Advanced Core Insulation: Closed-cell PU or high-density rock wool cores (70mm–100mm thickness) achieve thermal conductivity rates of ≤0.25 W/(m²·K), maintaining internal climate control in severe cold or tropical environments.
- Corrosion-Resistant Cladding: External structural panels feature fluorocarbon-treated galvanized steel or aviation-grade aluminum sheets, delivering robust protection against rust, salt atmospheric spray, and ultraviolet radiation.
- Integrated Weatherproofing: Built-in roof gutter networks combined with full-perimeter EPDM rubber gaskets secure an IP65 waterproof seal against extreme rainfall and wind-driven water intrusion.
- Broad Utility Range: High-spec wall and roof configurations make these modular buildings suitable for workforce housing, remote mining camps, emergency disaster recovery units, and commercial eco-tourism developments.
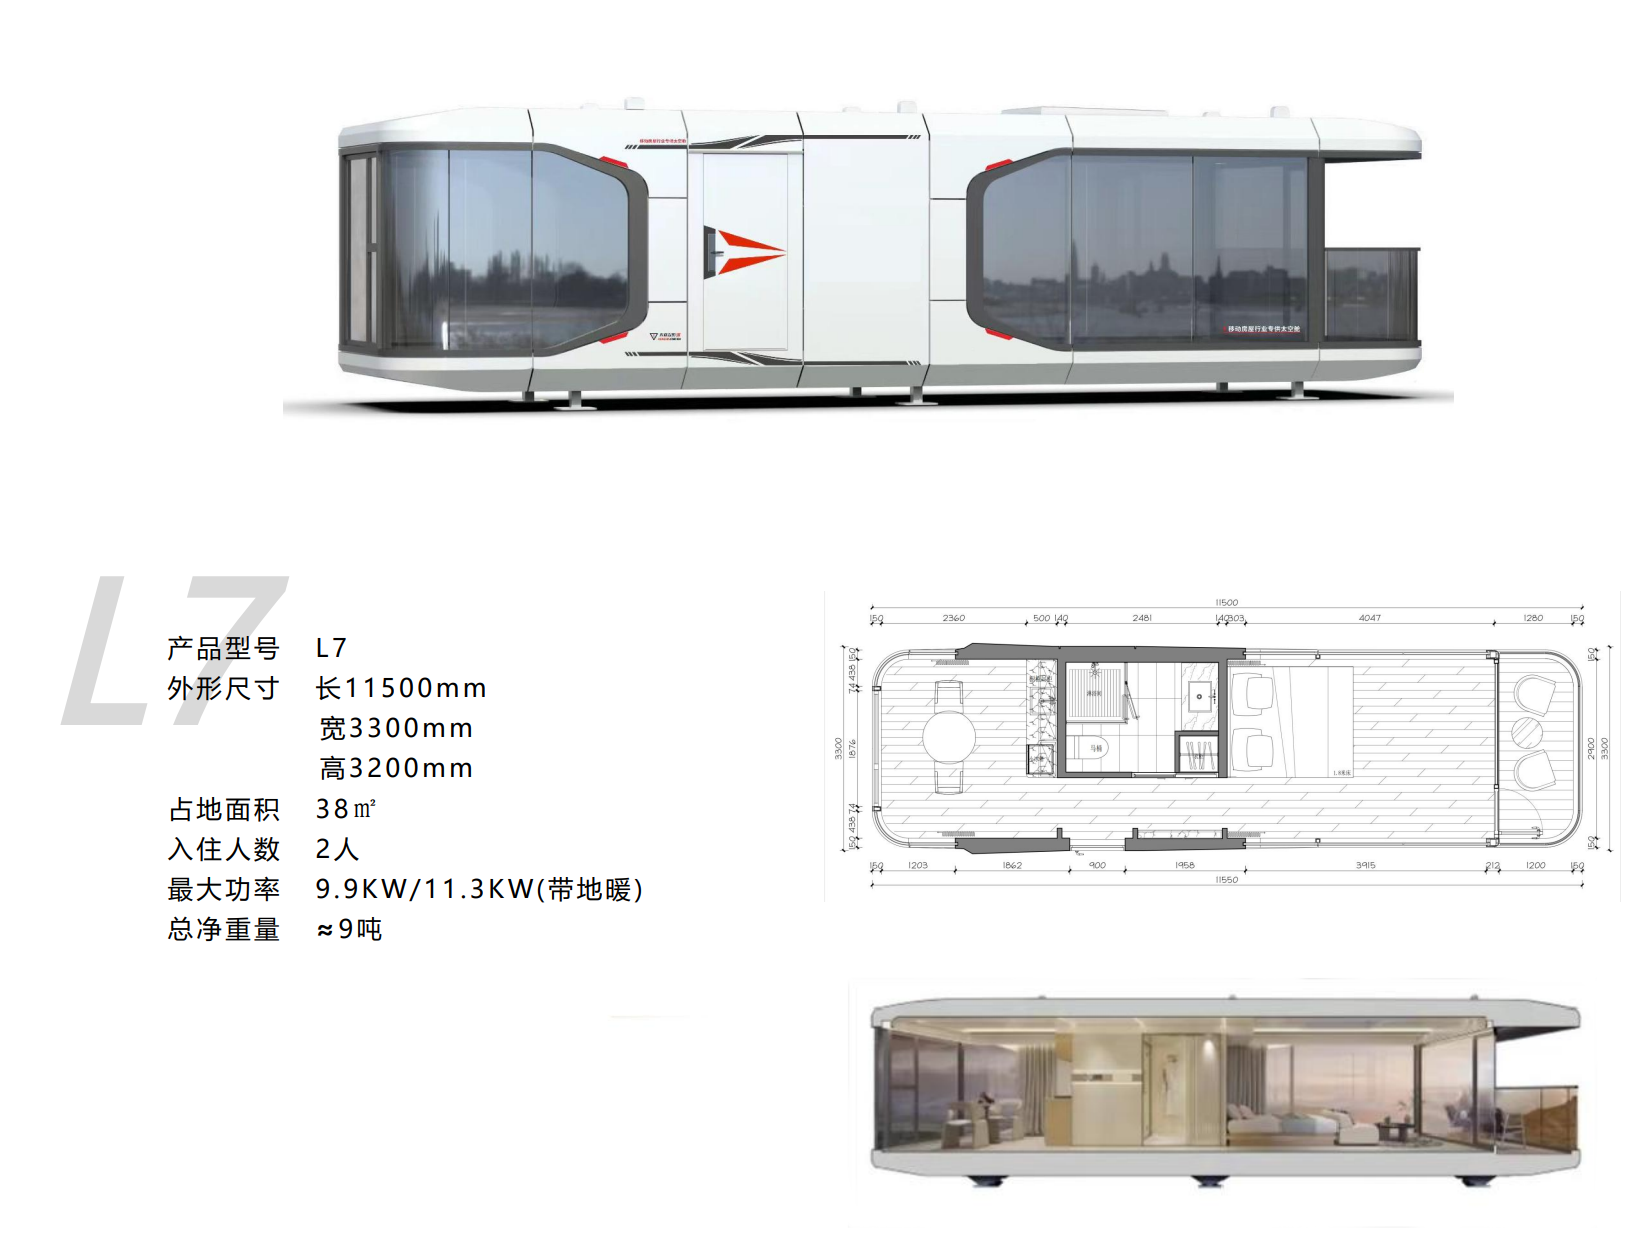
In-Depth Structural & Thermal Engineering Analysis
Analyzing wall and roof specifications requires examining structural framing, thermal efficiency, and water management. High-performance units utilize Q355 high-strength steel tubes for the primary framework. This steel undergoes pickling, phosphating, and electrostatic fluorocarbon coating processes to achieve resistance against Grade 10–12 winds and Grade 8 seismic activities. Wall panels are manufactured via automated continuous production lines, bonding outer metal skins with dense polyurethane or rock wool insulation to maximize thermal retention and acoustic dampening.
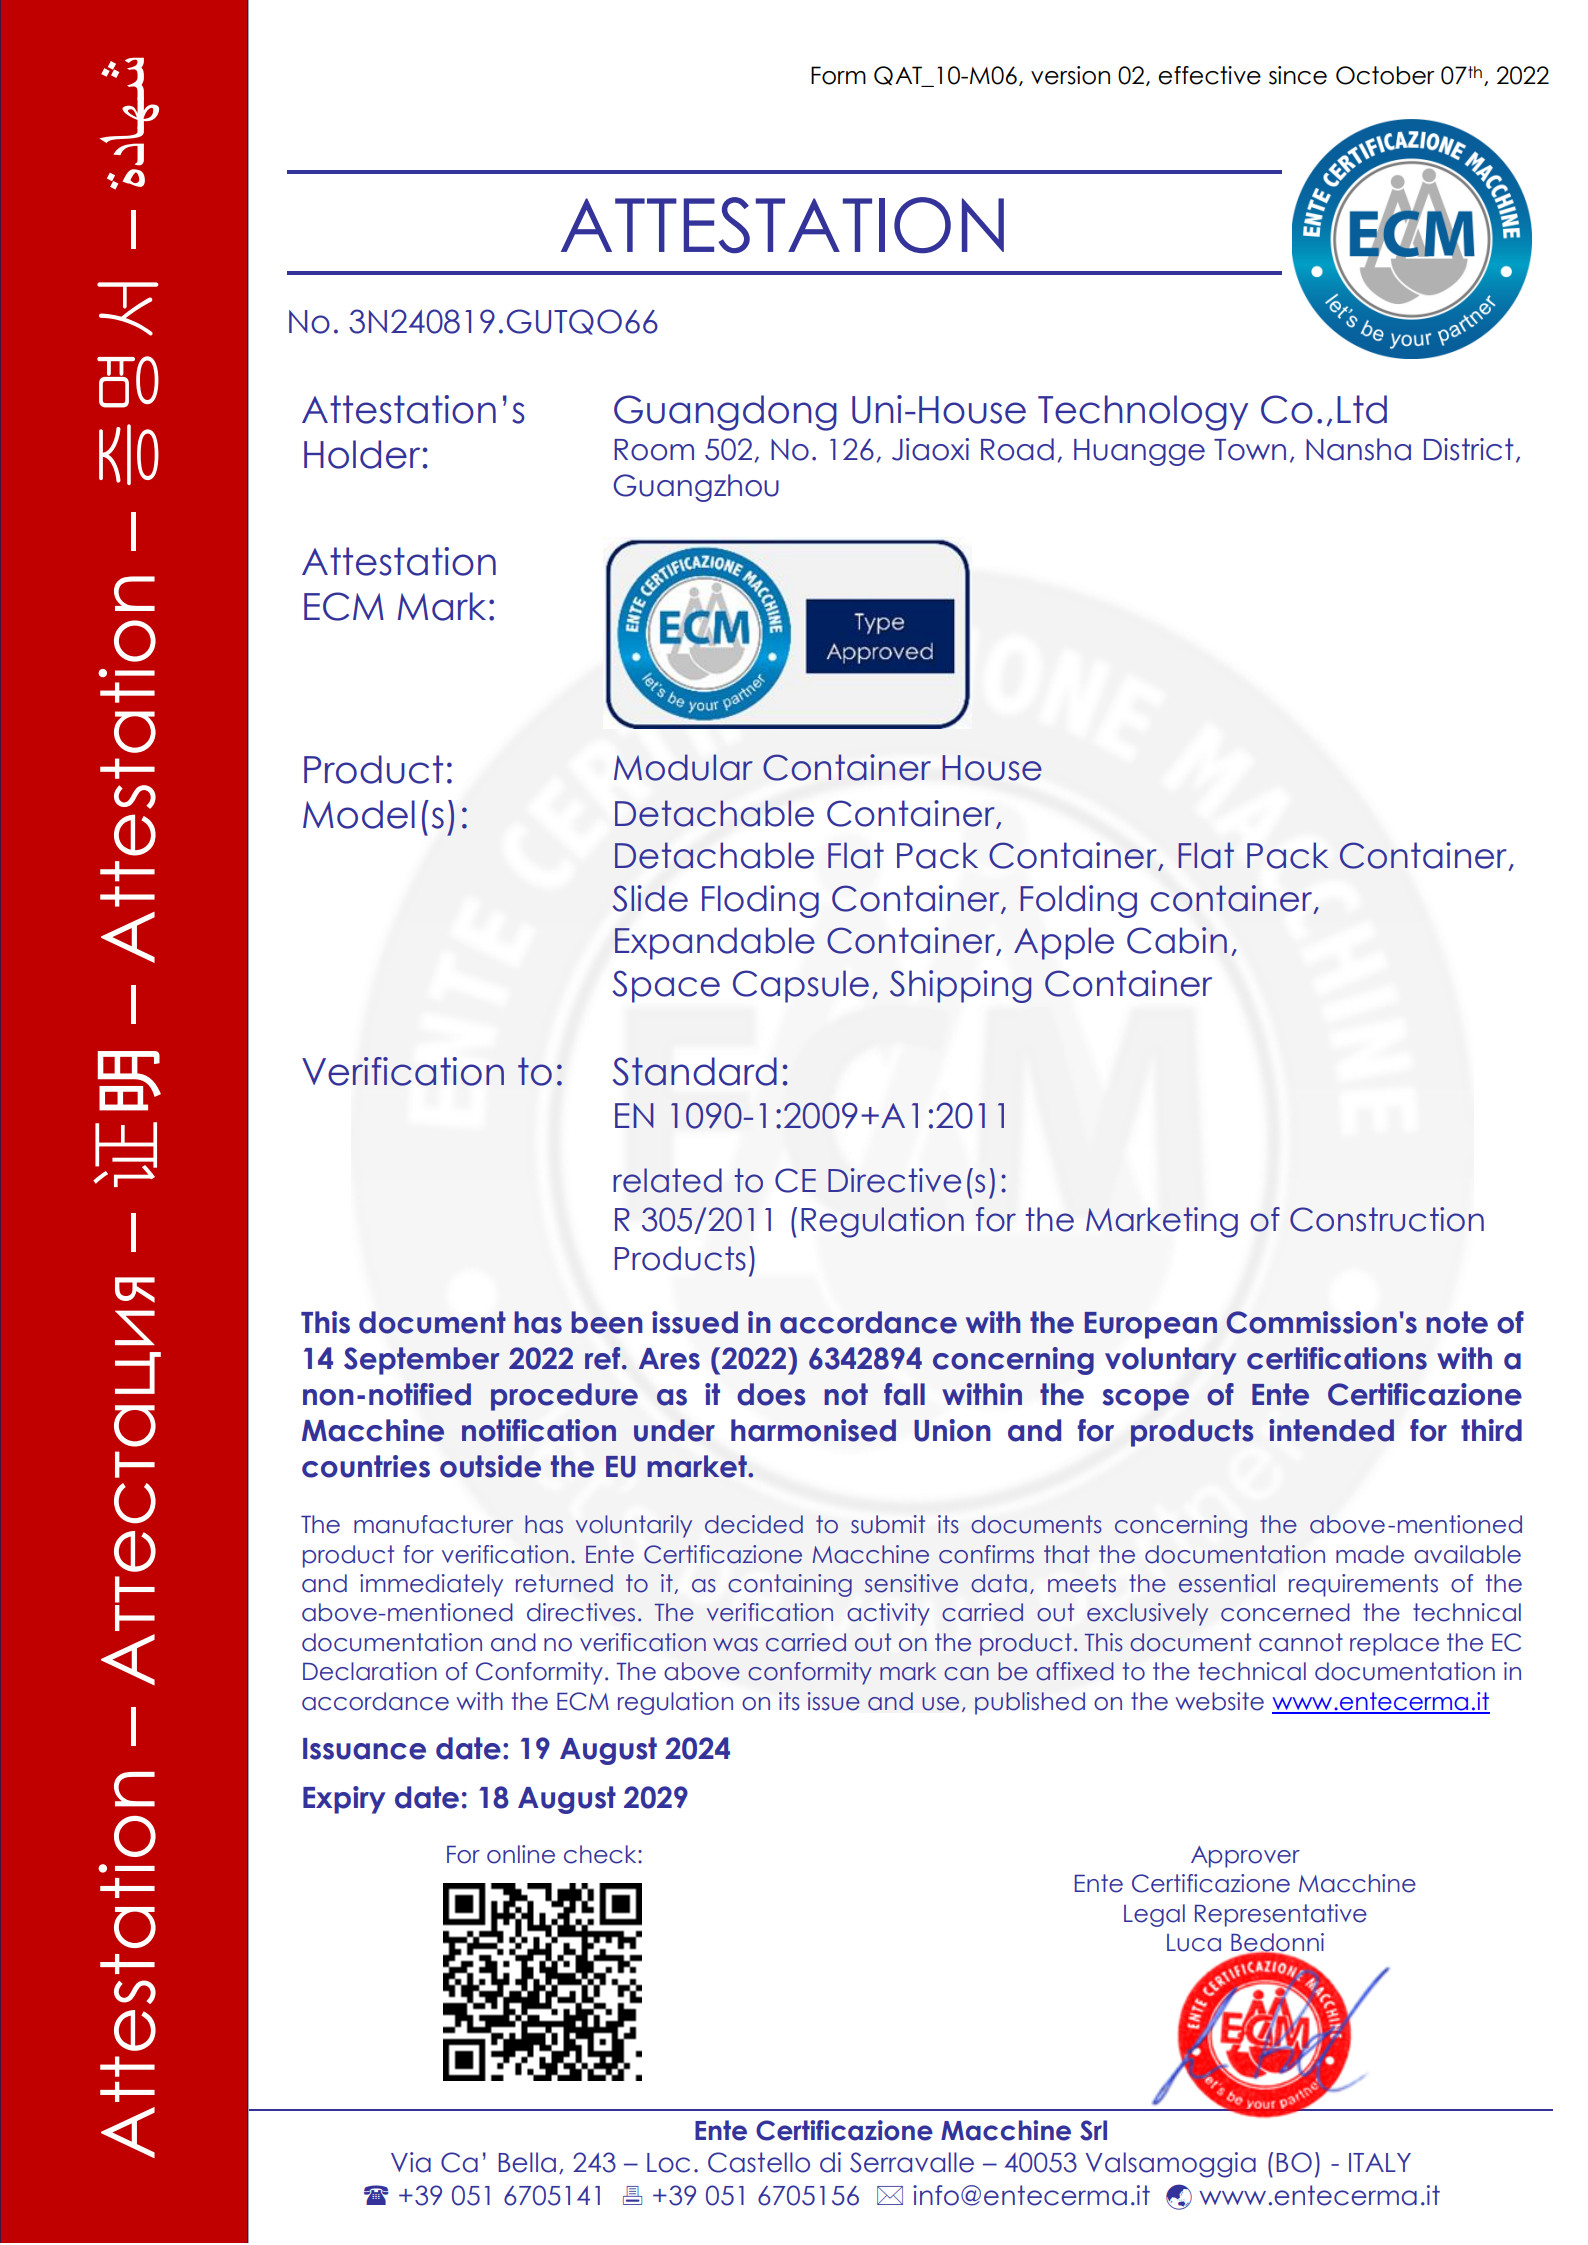
Roofing systems are engineered to resist structural fatigue while maintaining strict airtightness. Premium modular configurations feature embedded top drainage channels paired with double or triple-pane hollow insulated glass skylights, ensuring optimal natural light without breaking thermal barriers. Meeting rigid European safety standards, these container housing components hold official CE certification (No. 3N240819.GUTQO66), authorizing worldwide export across Europe, North America, Australia, and the Middle East.
Real-world deployments highlight the importance of modular structural design. For instance, in the Indonesian Coal Mine Living Area Project, 2,000 modular container dormitory units were established in a highly humid mining landscape. Insulated wall panels and leak-proof roof engineering delivered high indoor cooling efficiency and long-term durability throughout intense rainy seasons, enabling swift assembly and reducing operational costs.
Comparative Analysis of Wall and Roof Systems
Determining the right wall and roof specification depends on operational conditions, service life requirements, and site climates. Below is a structural comparison of common modular panel choices:
| Engineering Feature | Standard EPS Sandwich Panel | High-Performance PU / Rock Wool Panel | Heavy-Duty Aviation Aluminum Monocoque |
|---|---|---|---|
| Insulation Thickness | 50 mm – 75 mm | 70 mm – 100 mm | 70 mm – 100 mm (PU Core) |
| Thermal Conductivity Rate | Standard Performance | ≤0.25 W/(m²·K) | ≤0.25 W/(m²·K) |
| Waterproof Rating | Standard Overlap Joint | IP65 Integrated Gaskets | IP65 Seamless Monocoque |
| Operating Temperature Range | -10°C to +40°C | -40°C to +50°C | -40°C to +50°C |
| Wind Load Tolerance | Grade 8 – 9 | Grade 10 – 12 | Grade 10 – 12 |
| Target Application | Standard site offices | Mining camps, dorms, relief shelters | Eco-resorts, commercial capsules |

Frequently Asked Questions
Which wall insulation performs best in coastal or humid environments?
Closed-cell polyurethane (PU) sandwich panels are ideal for high-humidity climates. Their non-porous structure prevents moisture absorption, eliminating mold risk and thermal degradation while providing IP65 protection.
How does container roof engineering prevent water penetration?
Superior roof systems combine sloped profiles, internal perimeter gutter channels, factory-welded steel frame connections, and continuous EPDM seals rather than rely on simple overlapping sheets.
Can preassembled wall and roof units be transported efficiently overseas?
Yes. Detachable and flat-pack container wall and roof panels pack into compact, standardized bundles. These ship seamlessly in standard 20FT or 40HQ ocean containers for rapid onsite unloading by crane.
Summary & Buying Recommendations
Choosing high-density core panel insulation, robust anti-corrosion exterior coatings, and engineered internal roof drainage ensures long-term climate resilience, energy savings, and fire protection. Selecting panel specifications tailored to local wind, humidity, and thermal demands minimizes maintenance expenses over time. Under an integrated manufacturing-and-trade model, custom orders support flexible terms (minimum order quantity of 1 set) with a 50% deposit and 50% balance prior to shipment, dispatched in standard shipping containers. For technical consultations and customization requests, contact us at guizugroup@outlook.com.
Company Profile
Guangdong Uni-House Technology Co., Ltd. is a leading modular housing enterprise operating under the Guizu Group. Founded in 2008, the company employs over 200 specialists across a 30,000-square-meter facility with an annual manufacturing capacity of 10,000 sets. Equipped with automated sandwich panel lines, laser cutting machinery, robotic welding, and automated spray lines, the business delivers detachable container homes, flat-pack units, prefab K-houses, space capsules, and bespoke OEM/ODM solutions. All structures comply with international CE safety standards, serving clients across North America, Southeast Asia, Australia, and the Middle East.
REPORT