




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Audit Handle Assembly Lines in Half Tang Cutlery Factories
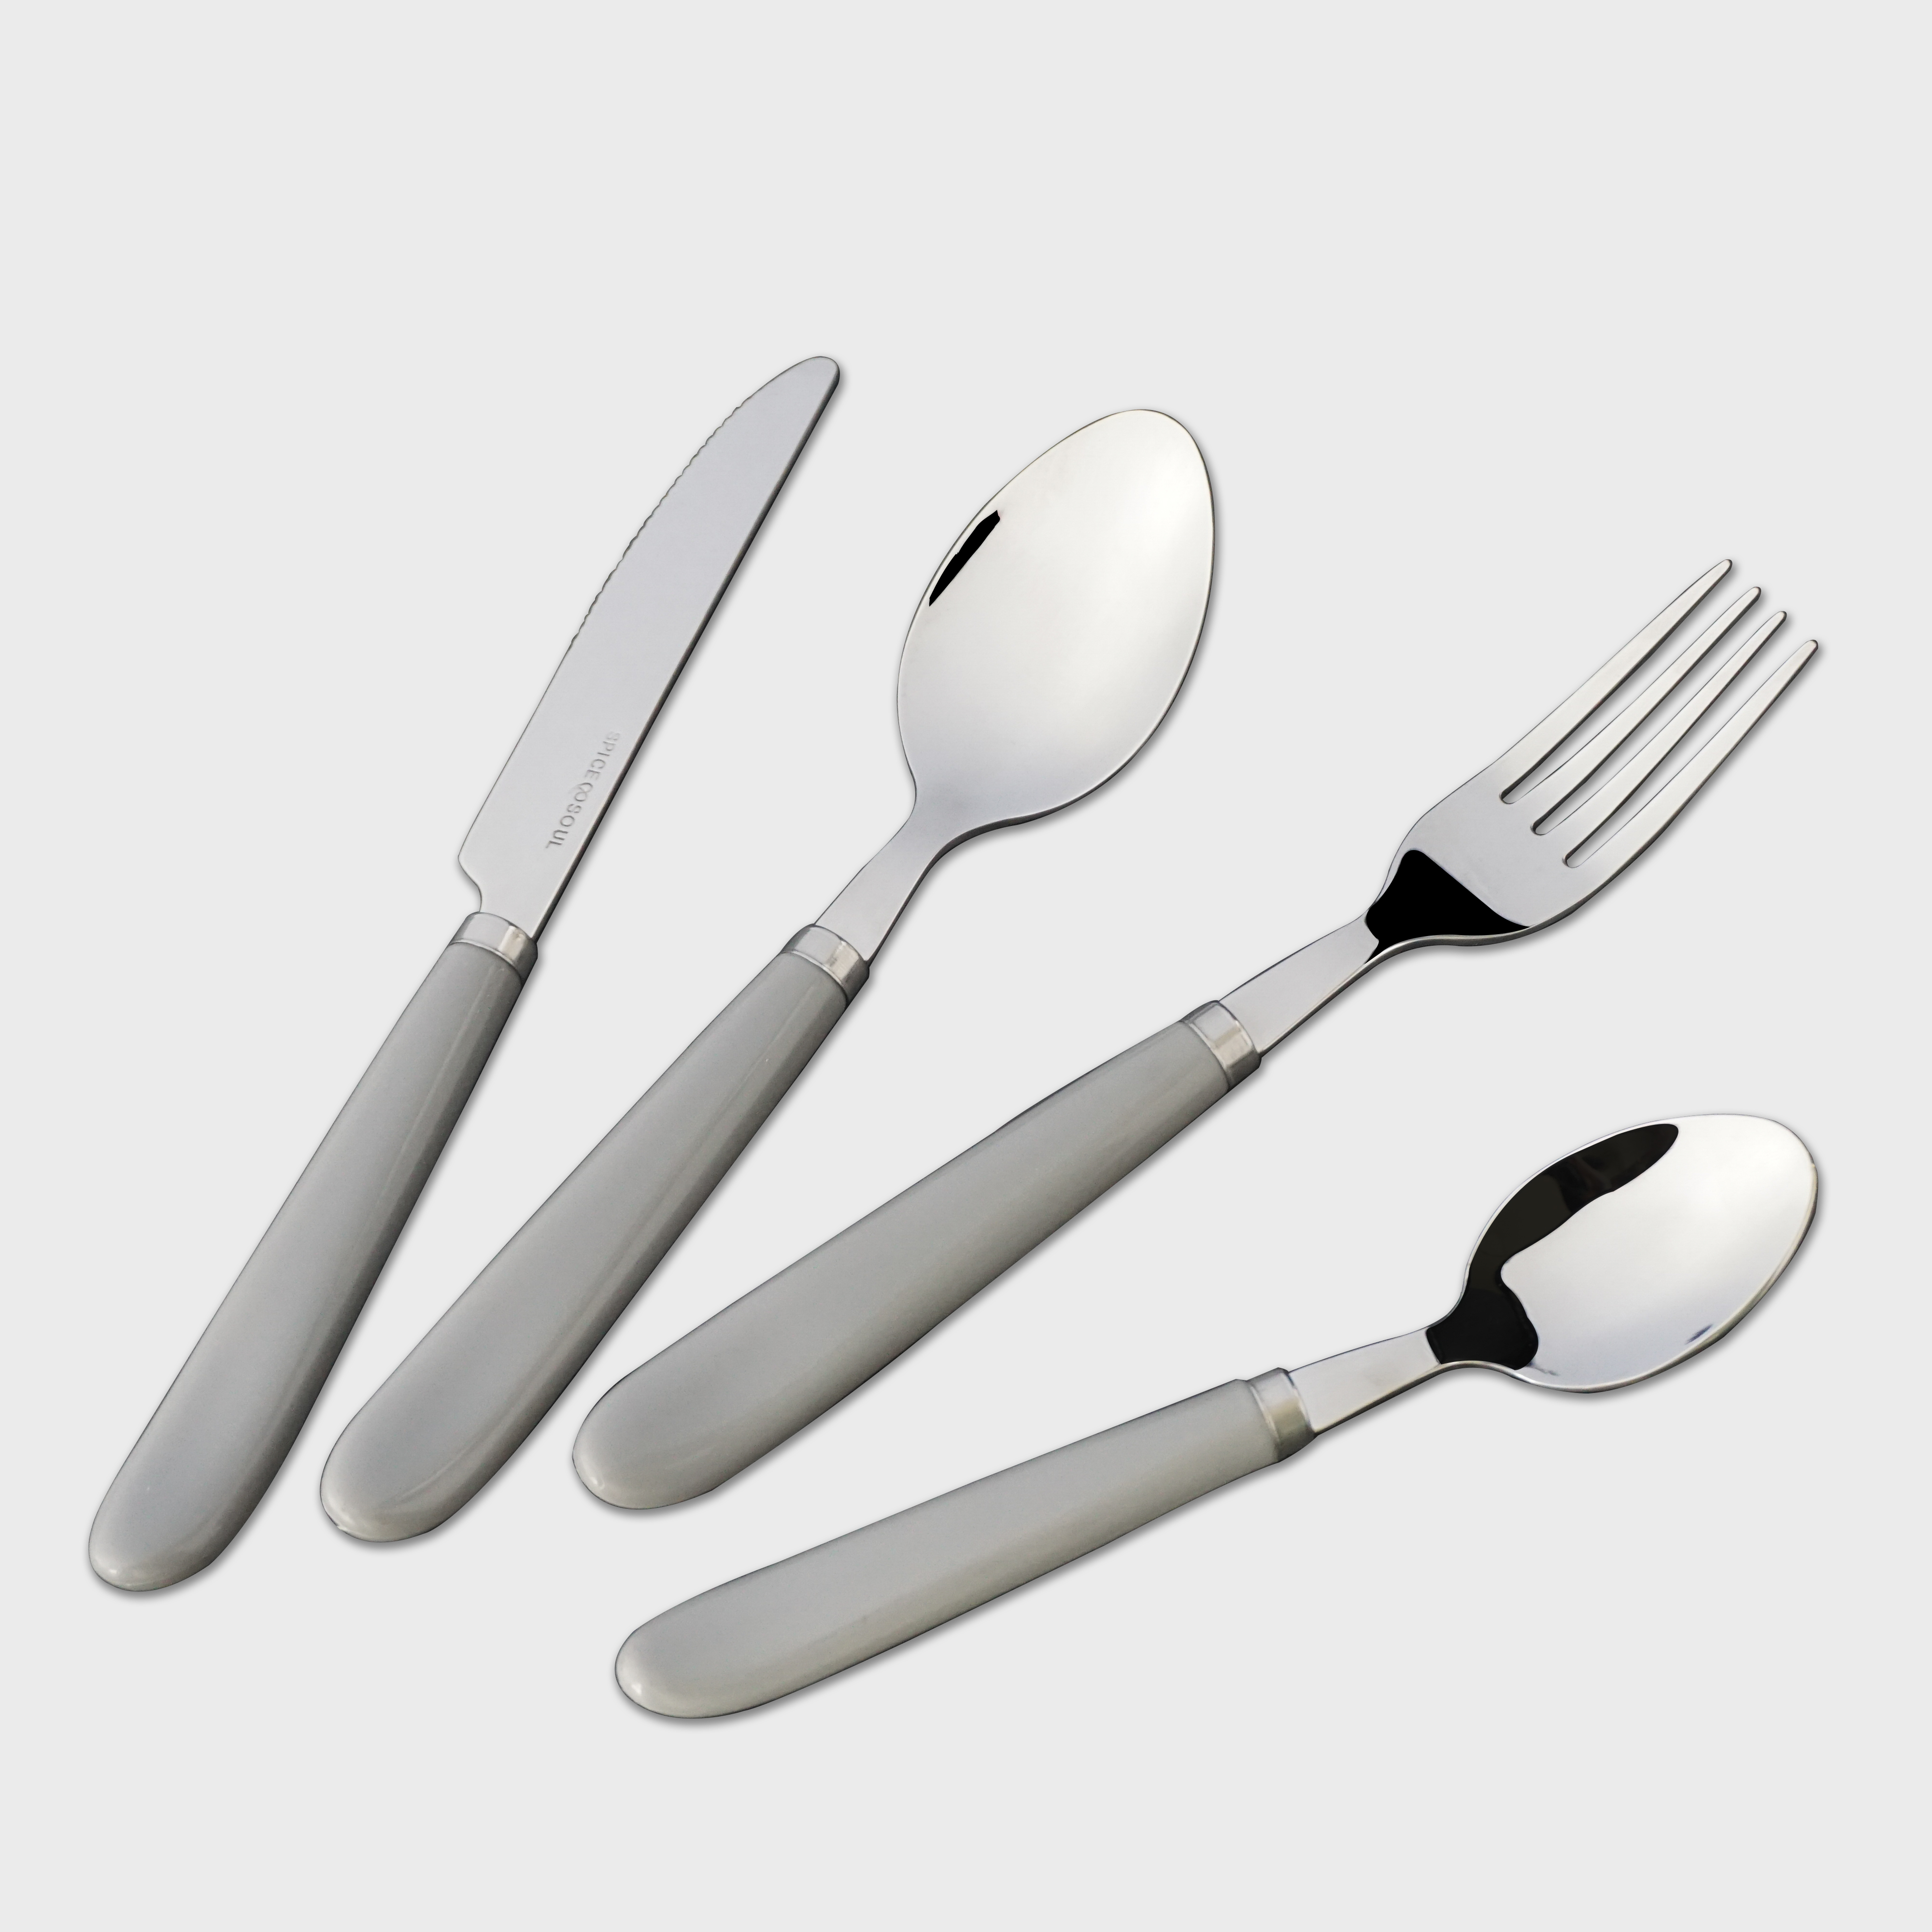
Handle assembly should be a dedicated focus during any audit of a half tang cutlery factory. Although the stainless steel component and plastic handle are produced through different operations, their final connection determines product stability, appearance, alignment, and service life. Auditors should observe molding, cooling, trimming, fitting, inspection, and packing while verifying that controls are applied consistently across production batches.
Why Handle Assembly Requires Direct Audit Attention
A half tang design depends on a reliable bond between the metal section and the handle. A loose fit, uneven alignment, molding flash, surface damage, or an unapproved material change can affect customer satisfaction and create problems during frequent use. This is particularly important for cutlery supplied to supermarkets, hotels, restaurants, and catering operations.
The audit should trace the complete product route, beginning with incoming stainless steel and plastic materials and continuing through injection molding, assembly, final inspection, and shipment. Comparing current production with approved samples helps determine whether the factory is maintaining the required handle geometry, color, finish, and assembly standard.
Key Audit Checks for Half Tang Cutlery
1. Injection molding and material control
Review whether food-grade ABS plastic is properly identified, stored, and issued to production. Inspect the injection molding process for stable settings, consistent handle dimensions, controlled cooling, clean trimming, and accurate formation around the metal component. The auditor should also confirm that production operators follow current work instructions and that any material or color changes receive formal approval.
2. Metal-to-handle fit and alignment
At the assembly station, examine whether the metal part is positioned correctly before the handle is completed. Finished samples should have a firm connection, even alignment, and no obvious gap between the two components. Check for looseness, deformation, exposed metal edges, flash, scratches, coating defects, and inconsistent transitions. Where possible, review the factory’s detachment or strength checks and confirm that the results are recorded by batch.
3. Appearance and finished-product inspection
Final inspection should cover both functional assembly quality and visual presentation. Sampling plans need to define inspection frequency, acceptance criteria, defect classification, and release authority. Records should show rejected quantities, the nature of defects, rework decisions, and the approval of products before shipment. A single attractive sample is not sufficient evidence; samples from multiple production batches should be reviewed.
Documentation, Traceability, and Corrective Action
Factory records should connect raw material receiving, molding, assembly, final inspection, and packing. Review material certificates or purchase records, production inspection reports, assembly checklists, appearance inspection forms, and shipment release documents. These records should make it possible to identify the production batch, responsible operators, inspection results, and any disposition of nonconforming products.
Complaint handling is another important part of the audit. The stated service process includes free replacement or refund for batch quality problems and a 24-hour response to customer complaints. Verify whether complaints are linked to defect analysis, affected batch numbers, containment actions, root-cause investigation, and documented corrective measures. This shows whether the factory can respond effectively when a recurring assembly issue is discovered after delivery.
Production Capability for Commercial Applications
For large-chain retail, hotel supply, restaurants, and catering replenishment, the factory must demonstrate repeatable assembly rather than occasional sample quality. Observe whether operators use suitable fixtures, standardized procedures, and controlled sampling methods. The available product information identifies plastic-handle cutlery for supermarket programs and tight injection molding for high-frequency restaurant and catering applications.
The operation is also described as supporting OEM and ODM production, private-label requirements, logo engraving, and customized packaging. These capabilities should be assessed together with the factory’s ability to preserve the approved design during volume production. Reported cooperation includes a German discount supermarket and European retail and homeware customers, but current controls at the specific manufacturing site still require on-site verification.
Audit Evidence Comparison
| Audit Focus | Documents or Evidence | Expected Confirmation |
|---|---|---|
| Plastic handle molding | ABS material records, molding instructions, machine or process logs, and in-process checks | Stable handle shape, controlled material use, clean surfaces, and repeatable molding results |
| Assembly connection | Approved reference samples, fixtures, operator instructions, and batch inspection records | Secure attachment, accurate alignment, and no visible gaps, looseness, or detachment risk |
| Visual quality | Sampling plans, appearance reports, defect classifications, and release approvals | Flash, scratches, deformation, coating problems, and assembly defects are identified before shipment |
| Certification and compliance | BSCI, ISO9001, LFGB, and FDA documents applicable to the factory or product | Certificate scope, validity, product coverage, and manufacturing site are consistent |
| Post-delivery response | Complaint records, response timelines, replacement or refund files, and corrective-action reports | Quality issues are traceable, contained, investigated, and resolved systematically |
Frequently Asked Questions
Should handle assembly and metal processing be audited as separate operations?
Yes. Each operation presents different risks and should be reviewed independently. The audit should then confirm that the completed product has the correct fit, alignment, appearance, and resistance to loosening or separation.
What are the most important quality points for a half tang handle?
Check the metal-to-handle connection, dimensional consistency, alignment, gap size, molding flash, surface condition, firmness, and agreement with approved samples. Assembly instructions and final inspection records should be reviewed alongside physical samples.
Do BSCI, ISO9001, LFGB, or FDA documents remove the need for an assembly-line inspection?
No. These documents provide useful evidence of management systems, social responsibility, or product compliance, but they cannot replace direct observation of current molding, assembly, inspection, traceability, and corrective-action practices.
Conclusion and Practical Recommendation
Yes, the handle assembly line should be inspected when auditing a half tang cutlery factory. Give priority to food-grade ABS control, injection molding consistency, metal-to-handle positioning, secure attachment, appearance standards, batch traceability, and complaint-related corrective action. Reviewing several production batches and matching physical findings with factory records provides a more reliable assessment than checking certificates or one finished sample alone.
JIEYANG CITY HUAQIANG METAL INDUSTRY CO., LTD. is described as a direct factory supplier offering standard production and OEM/ODM customization. For technical questions or production support, contact eyas2018@126.com.
About the Manufacturer
JIEYANG CITY HUAQIANG METAL INDUSTRY CO., LTD. manufactures stainless steel tableware and kitchenware in Jieyang City, Guangdong Province. The company reports 40 years of industry involvement and more than 16,000 square meters of production space. Its capabilities include OEM/ODM services, logo engraving, customized packaging, an internal mold workshop, and integrated support from product design through mass production.
The production range includes full tang cutlery, half tang products, plastic-handle and colorful cutlery, and kitchen tools. The company states that it holds BSCI and ISO9001 certifications and serves customers in multiple industries.
REPORT