




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Confirm an SPR Riveting Gun Sample Is Ready for Mass Production
Approving an SPR riveting gun for mass production requires more than checking its appearance or running a brief demonstration. The sample should be compared with the promised production configuration, tested under the intended joining conditions, and supported by traceable inspection records. Key checks include the claimed 30–60 kN output range, accurate pressure control, functional performance, application results, delivery terms, and after-sales support.
Production Approval Checklist
- Confirm that the SPR riveting gun delivers the specified 30–60 kN output pressure and that its adjustment mechanism operates consistently across the range.
- Ask for sample-specific inspection documentation, including functional test results completed before shipment.
- Evaluate the joining process using the actual materials, stack-ups, and components planned for production, such as aluminum vehicle structures, EV battery trays, or water cooling plates.
- Compare the tested sample with the proposed production version, including its configuration, tooling, validation results, lead time, and support arrangements.
How to Evaluate the Sample
1. Verify the Main Performance Parameters
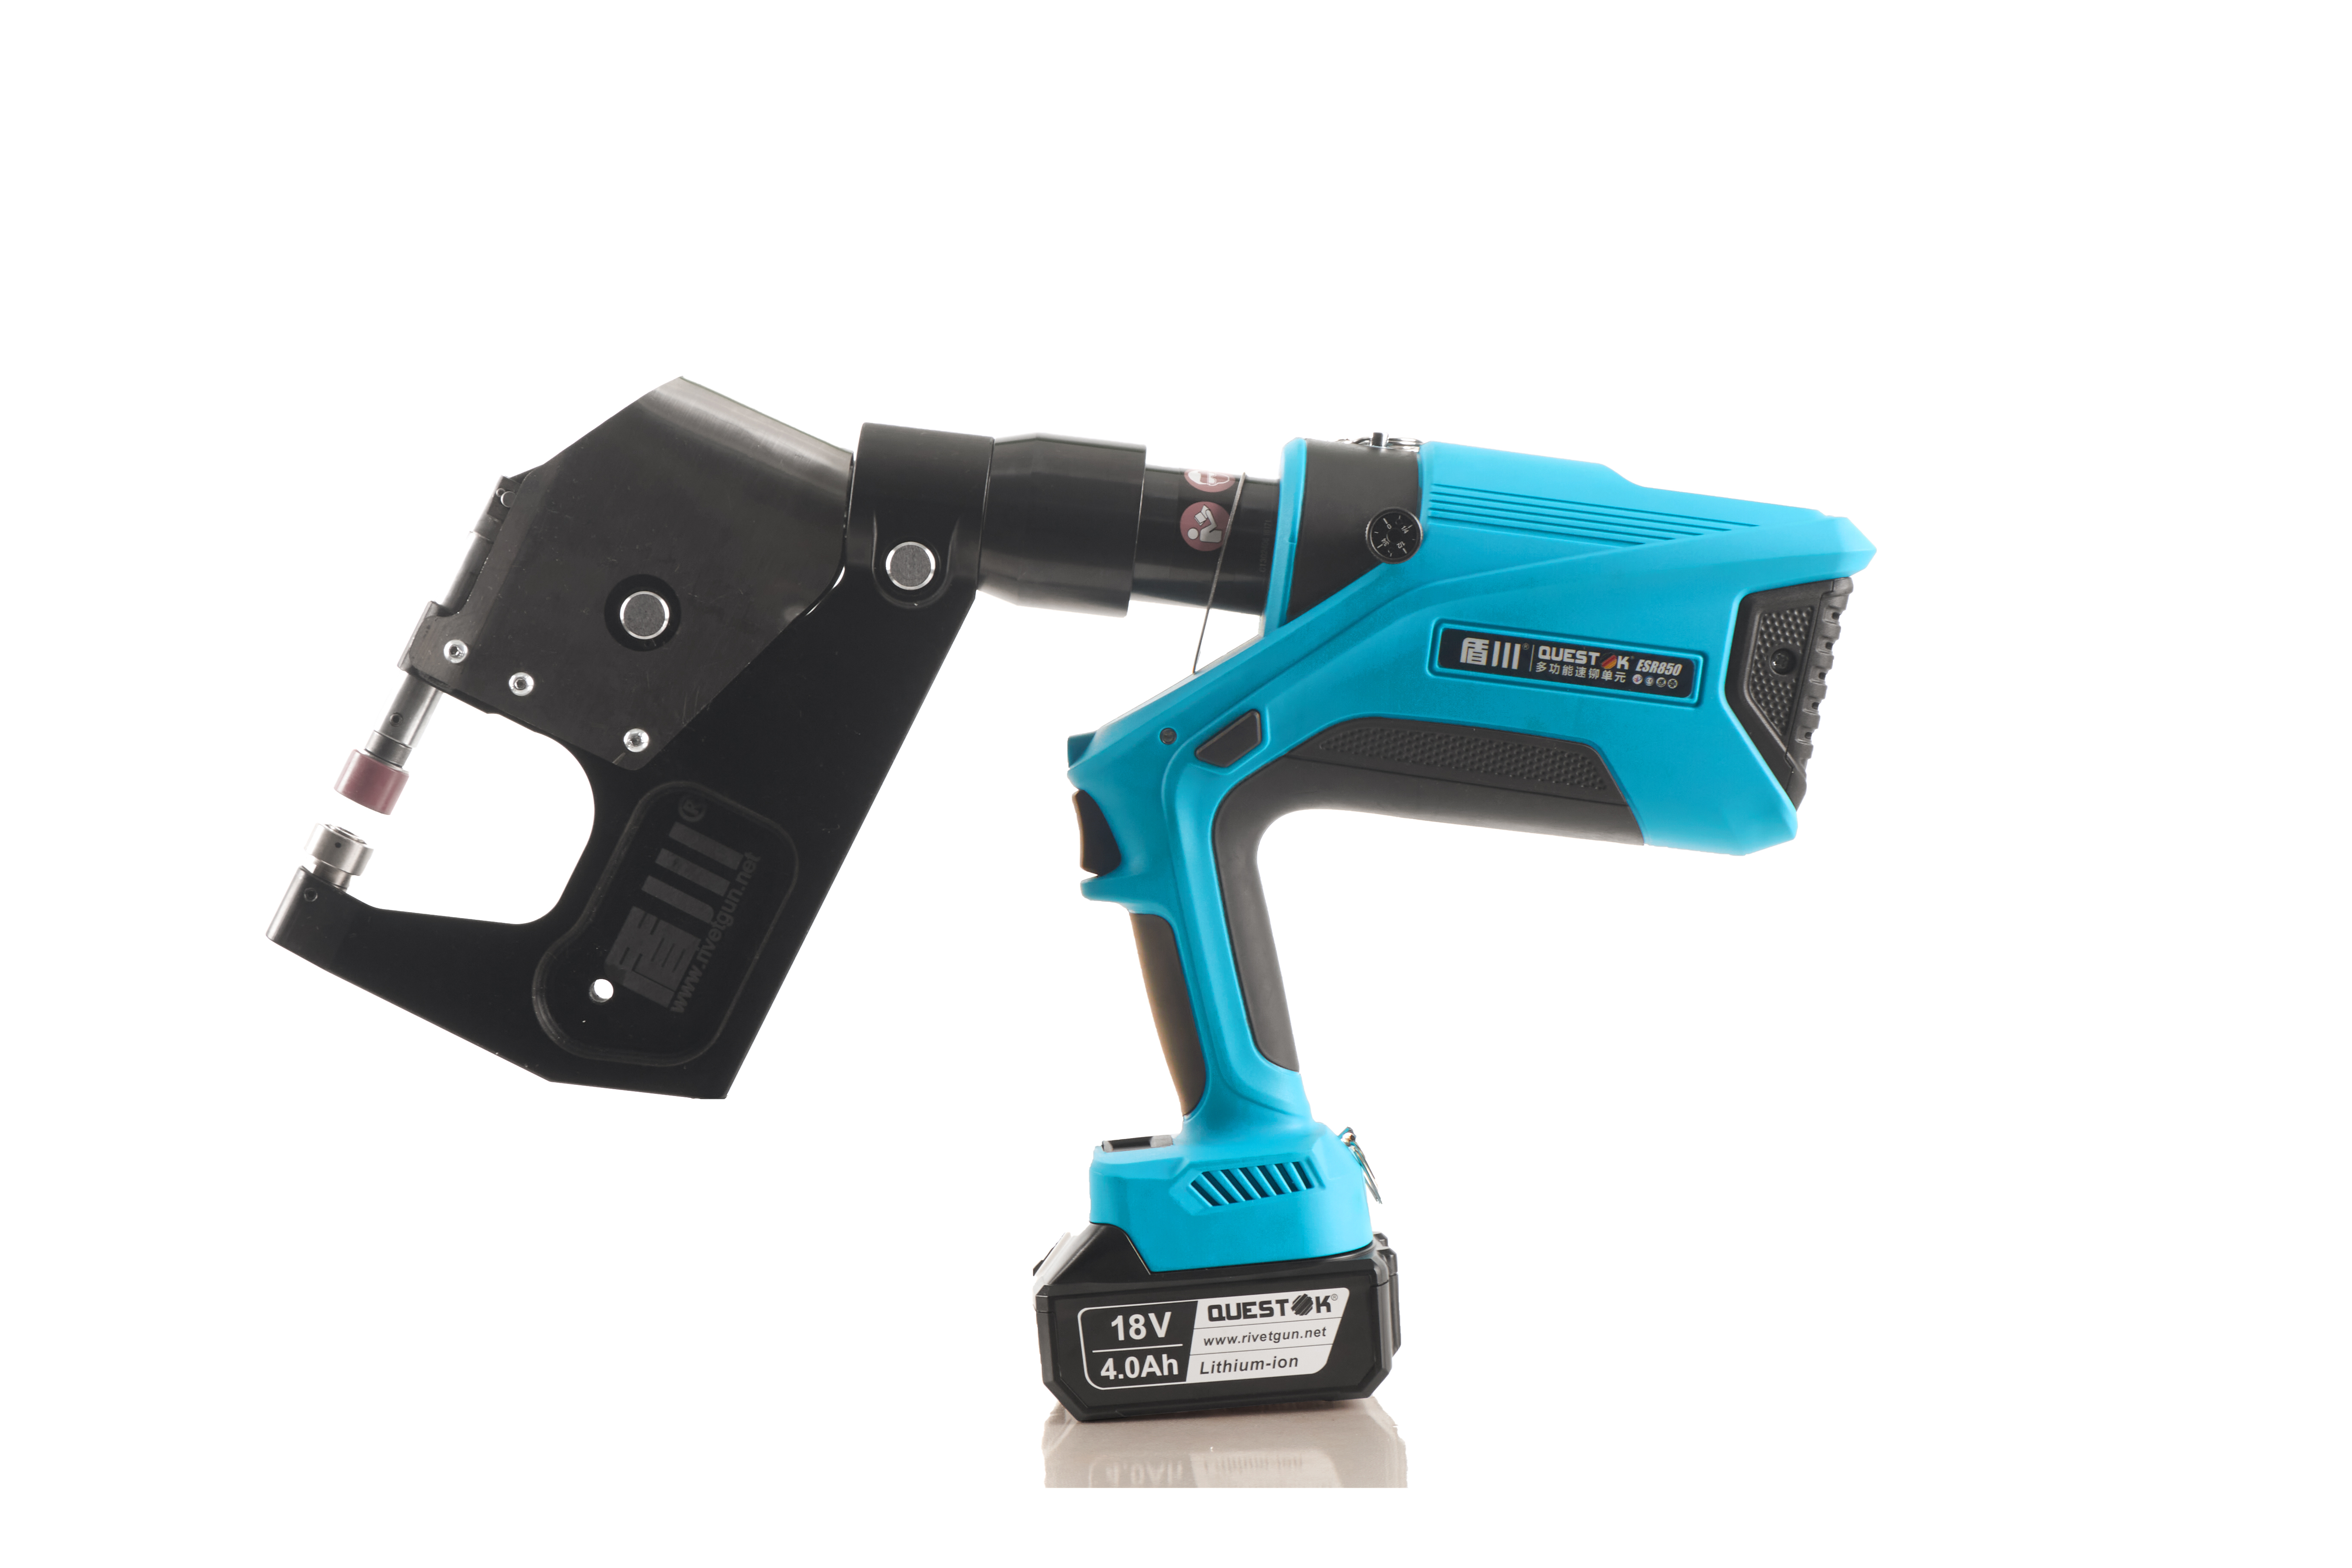
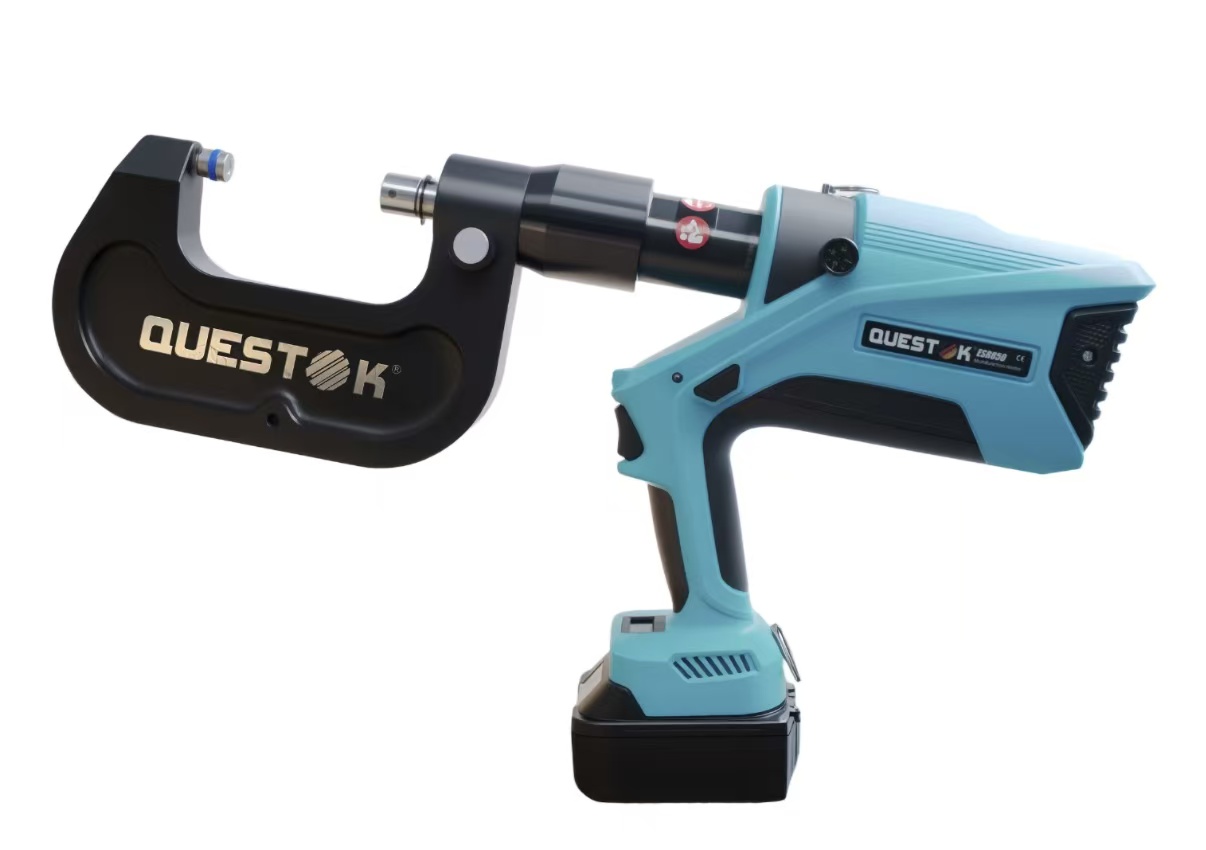
The SPR riveting gun is designed for sheet metal joining and is specified with an output pressure of 30–60 kN. The pressure is described as precisely adjustable, making this range the first technical reference for sample approval. Record the setting used in the supplier demonstration, then check whether the delivered unit provides the same adjustment behavior.
Pressure capability alone does not prove production readiness. The customer should determine whether the force remains stable during repeated cycles and whether the tool can produce consistent joints under the planned operating conditions. The sample should therefore be tested with the same material combinations and process requirements expected on the production line.
2. Link Inspection Evidence to the Delivered Unit
Supplier quality statements should be supported by records that identify the specific sample under review. Questok states that it performs full inspection and checks materials, manufacturing processes, and completed products against internal standards. Functional testing is also reported to take place before delivery, with test photos and videos available for customers.
Request the applicable inspection checklist, functional test results, serial number or configuration details, and any available visual evidence. These documents help establish whether the sample tested by the supplier is the same model and configuration proposed for mass production. They also provide a reference if performance questions arise after installation.
3. Validate the Intended Joining Application
An SPR tool should be approved through the complete joining process rather than through a catalog specification alone. Questok reports applications in automotive manufacturing, EV battery trays, and water cooling plates. The sample should be assessed with the customer’s actual sheet materials, thicknesses, surface conditions, rivets, dies, and access limitations.
Application testing should include joint appearance, joint strength, repeatability, dimensional requirements, and any destructive or metallographic analysis required by the customer. A generic demonstration may show that the tool functions, but only an application-specific trial can establish whether it is suitable for the planned assembly.
Configuration, Customization, and Support Review
Before issuing production approval, compare the sample with the process documentation and commercial commitment. Confirm the tool identity, pressure range, adjustment method, accessories, control system, tooling, inspection status, and test results. For a standard model, ensure that the unit tested is configured in the same way as the units to be ordered.
Customized projects require an additional comparison. The supplier states that customized production can be completed in 15 days and supports ODM and OBM cooperation with a minimum order quantity of one set. The customer should document the required material combination, joining sequence, tooling, cycle conditions, and acceptance criteria, then verify that the tested sample represents the final proposed solution rather than an interim prototype.
Reported project experience also shows why engineering validation may be necessary. In an EV vehicle prototype project, the supplier visited the customer’s factory, reviewed requirements with engineers, and developed a dedicated SPR system following application evaluation. In another automotive project involving complex combinations of high-strength materials, the reported process included repeated trials, metallographic analysis, test records, and die modifications before approval. These examples indicate that demanding applications may require iterative process development.
Verification Data Comparison
| Review item | Supplier information | Recommended customer check |
|---|---|---|
| Pressure output | 30–60 kN with precise adjustment | Measure the delivered tool’s operating range and confirm stable adjustment under repeated use. |
| Inspection process | Full inspection from materials through finished products | Obtain inspection records and connect them to the sample’s serial number or configuration. |
| Functional testing | Functional checks are completed before delivery; photos and videos may be provided | Review sample-specific test evidence and repeat key checks at the customer’s facility. |
| Application coverage | Automotive production, EV battery trays, and water cooling plates | Run trials with the actual materials, components, rivets, tooling, and production conditions. |
| Standard delivery | Three days after payment for orders below 50 sets | Confirm that the quoted lead time and configuration apply to the exact standard model required. |
| Customized delivery | Fifteen days for customized solutions | Verify that the approved sample reflects the final customized design and process requirements. |
| After-sales service | Global product response within 24 hours, with troubleshooting and spare-parts support | Clarify communication channels, spare-parts availability, escalation procedures, and service coverage. |
Certification and Documentation
The company lists CE certifications for its SPR riveters, SPR riveting guns, SPR riveting systems, self-piercing riveting guns, and related joining equipment. It also lists an MSDS certificate for the relevant product group. Before shipment or production use, check that the certificate title, product scope, model, and destination-market requirements match the exact sample being evaluated.
Frequently Asked Questions
What should be checked first on an SPR riveting gun sample?
Begin with the stated 30–60 kN output pressure and the precision of the pressure-adjustment function. These are the primary published performance indicators and should be confirmed before moving to full application testing.
Can a supplier’s inspection declaration alone support mass-production approval?
No. The supplier reports full inspection and pre-delivery functional testing, but the customer should review records tied to the actual sample and validate the joining process with production materials and components. Documentation and application results address different quality risks.
How should a customized SPR solution be approved?
Define the materials, assembly design, tooling, process parameters, and acceptance criteria in advance. Then confirm that the tested sample includes the same customized configuration intended for production. The supplier reports a 15-day customization period and supports orders of one set.
Final Recommendation
An SPR riveting gun sample should be considered for mass production only after its pressure capability, adjustment accuracy, repeatability, inspection records, functional test evidence, and application-specific joining results have been confirmed. Review the applicable CE certification scope, match the sample configuration to the production proposal, and establish the service and spare-parts process before deployment. For technical consultation or customized joining support, contact jane@questok.com.
About PHOTON TECHNOLOGY KUNSHAN CO.,LTD
PHOTON TECHNOLOGY KUNSHAN CO.,LTD, operating under the Questok brand, develops fastening, joining, and assembly equipment for modern manufacturing. Founded in 2011, the company reports an engineering team with more than 10 years of experience in SPR riveting systems, self-piercing riveting guns, clinching equipment, hydraulic and control systems, process validation, and reliability testing. Its stated capacity includes 800 standard sets and 500 customized sets, with customers across several industries. The company lists CE and MSDS certifications for relevant joining products.
REPORT