




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Lower Injection Mould Costs Without Compromising Part Strength
Lowering injection mould cost does not require sacrificing the performance or durability of the finished plastic part. The most effective approach is to align part geometry, cavity configuration, mold steel, surface finish, and runner technology with the actual production requirements. By removing nonessential complexity while protecting wall uniformity, functional tolerances, mold life, and inspection standards, manufacturers can control tooling investment without weakening the final product.
Practical Cost-Reduction Strategies
- Design consistent wall sections, usable draft angles, and fewer difficult features to reduce machining, fitting, and assembly work.
- Choose a single-cavity or multi-cavity mold according to forecast volume, cycle requirements, and tooling budget.
- Select mold steel, including S50C, P20, 1.2738, H13, or 718H, based on required service life, surface quality, and operating conditions.
- Specify SPI or VDI finishes only where appearance, texture, release, or function requires them.
- Consider hot runners as a production-specific option rather than treating them as an automatic cost-saving solution.
Design Principles That Protect Part Quality
Simplify the Geometry Where Possible
Part design is one of the strongest drivers of injection mould cost. Unnecessary ribs, deep pockets, abrupt transitions, sharp corners, and complex undercuts can increase CNC machining, EDM, mold assembly, and maintenance requirements. Removing or simplifying features that do not contribute to the product's function can reduce tooling effort while preserving the important interfaces and performance characteristics.
Uniform wall thickness helps limit sink marks, warpage, and uneven cooling. Practical draft angles also support reliable ejection and reduce the risk of damaging the mold or molded part during production. These changes should be reviewed against the required dimensional tolerances so that cost reduction does not affect fit, assembly, or operation.
Match Cavity Count to Production Demand
A larger cavity count is not always the most economical choice. For lower or uncertain volumes, a single-cavity mold may reduce the initial tooling scope and simplify sampling, maintenance, and dimensional adjustment. When demand is high enough, multi-cavity tooling can provide greater output and a lower molded-part cost, but it requires more precise cavity matching, balanced filling, and additional mold engineering.
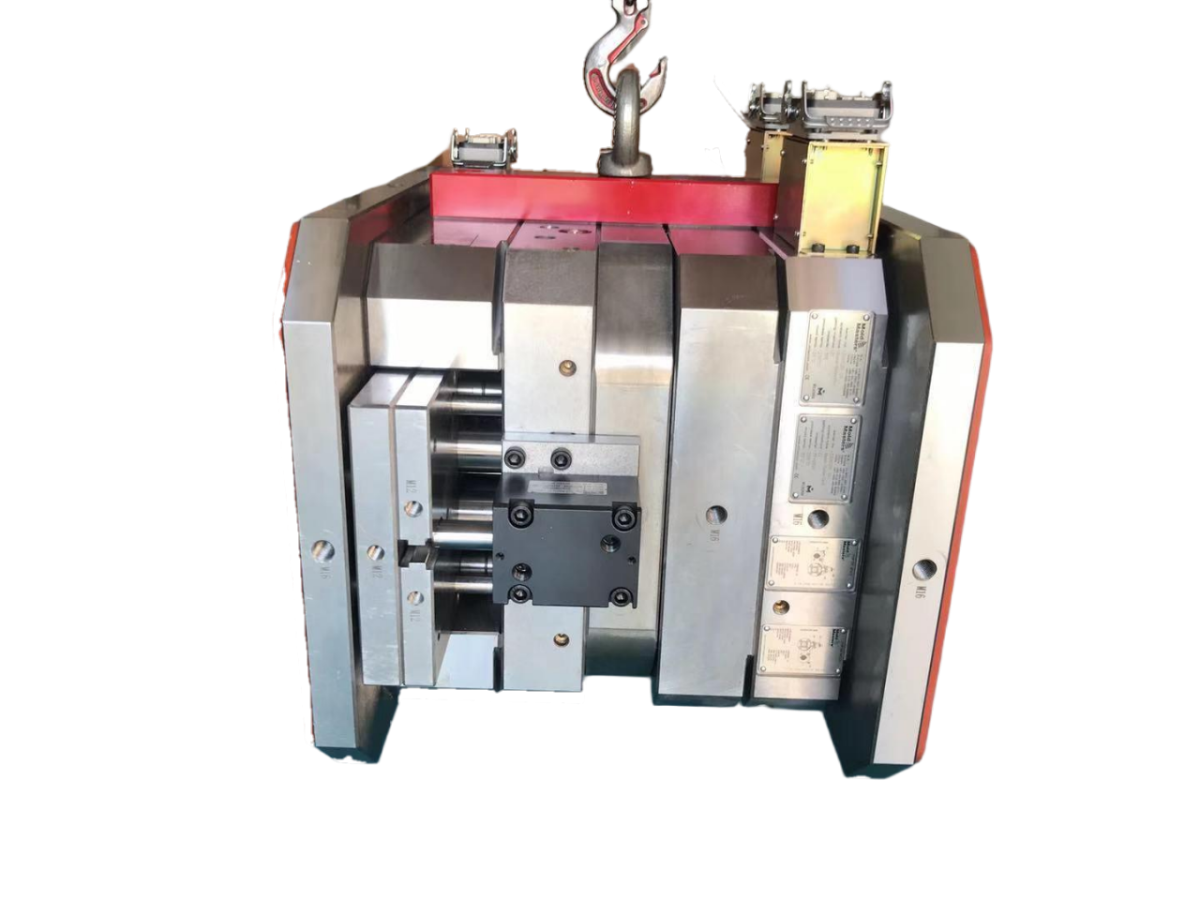
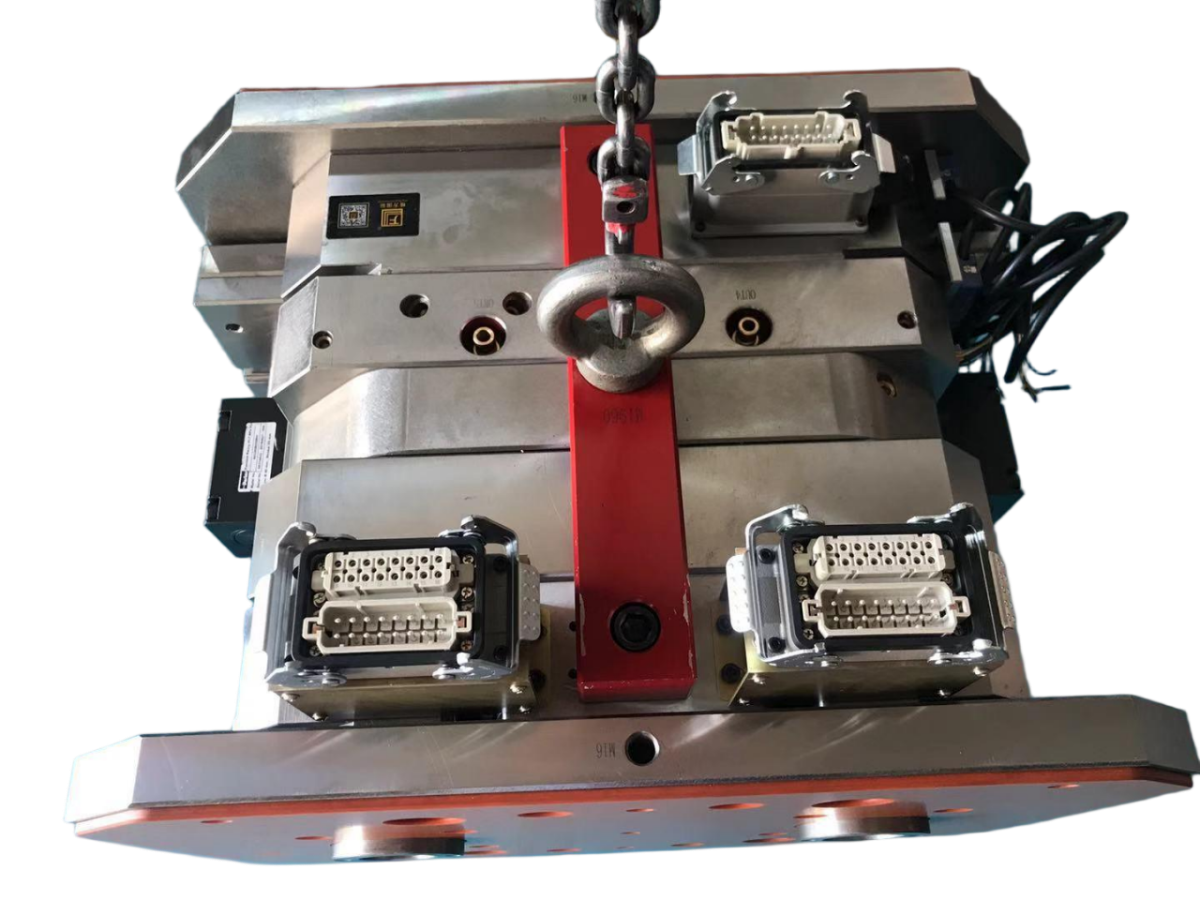
Longterm's custom precision plastic injection mould service supports both single-cavity and multi-cavity solutions, with mold lives ranging from 50,000 to 1,000,000 shots. The correct configuration depends on forecast output, part size, resin selection, cycle time, and the acceptable tooling investment.
Choose Mold Steel According to the Application
Mold steel should be selected according to actual production conditions rather than maximum specification alone. S50C may suit applications with moderate requirements, while P20, 1.2738, H13, or 718H can be considered when higher durability, polishing performance, heat resistance, or production volume is required. Matching the grade to the expected mold life prevents unnecessary material expense while maintaining production stability.
Surface treatment should follow the final part requirement. SPI or VDI finishes can be applied when the product needs a defined appearance, texture, release behavior, or functional surface. Avoiding an unnecessarily high finish level can reduce polishing and finishing work without changing the performance of the plastic component.
Evaluate Hot Runners as Part of the Full Mold Design
Hot runners can reduce cold-runner waste and may improve production efficiency in suitable high-volume applications. However, they also introduce additional system, control, maintenance, and troubleshooting requirements. The decision should consider annual volume, material cost, gate layout, cycle targets, resin behavior, and maintenance capability. A hot runner is cost-effective only when its production benefits justify the additional tooling scope.
Verification Keeps Cost Reduction Under Control
Tooling savings should always be checked against product quality and process reliability. Longterm identifies IQC incoming inspection, mold trial testing, dimensional inspection, and full inspection before shipment as part of its quality process. Its ISO 9001:2015 certification covers the design, manufacturing, and sales of precision molds, as well as the sales of plastic products.
Recorded cooperation projects include an electronic housing mold for an Italian manufacturer, a double-shot overmolding mold for a French product brand, a home appliance component mold for a US brand distributor, and an industrial equipment housing mold for an Australian manufacturer. Reported results included dimensional accuracy, smooth surfaces, correct alignment, stable trial samples, specification compliance, and resolution of technical issues.
Design Choices at a Glance
| Design option | How it can control cost | Quality condition to maintain |
|---|---|---|
| Single-cavity mold | Reduces initial tooling complexity and is practical for limited demand | Confirm that the output target and delivery schedule can be met |
| Multi-cavity mold | Increases production capacity and may lower the unit tooling contribution | Keep cavities dimensionally consistent and filling properly balanced |
| Simplified geometry | Limits difficult machining, fitting, ejection, and mold modification | Retain functional features, suitable draft, consistent walls, and tolerances |
| Application-matched steel | Controls material cost according to expected mold life and service conditions | Select S50C, P20, 1.2738, H13, or 718H according to the actual requirement |
| Hot runner system | Can reduce runner waste and support efficient high-volume production | Review gate design, resin behavior, controls, maintenance, and trial needs |
Frequently Asked Questions
Can a simpler mold still produce a high-quality plastic part?
Yes. Removing nonfunctional complexity, reducing difficult undercuts, and using suitable draft angles can lower tooling work while preserving the features, tolerances, and strength required by the product.
Is a multi-cavity mold always the best way to reduce part cost?
No. Multi-cavity tooling is useful when production demand is sufficiently high, but it increases design, machining, balancing, and maintenance requirements. Cavity quantity should be based on the forecast volume and total project economics.
How should surface finish be selected when appearance is important?
Specify the SPI or VDI level required by the product instead of choosing the highest available finish by default. The finish should be evaluated with the part appearance, mold steel, release requirements, and manufacturing process.
Conclusion
The most reliable way to reduce injection mould cost is to remove unnecessary complexity while keeping the features that support strength, fit, appearance, and production performance. Use consistent walls and practical draft, select cavity count according to demand, match mold steel to the expected service life, specify only the necessary surface finish, and review hot runners as part of the complete tooling strategy.
Longterm provides OEM custom plastic injection molds, custom mold making with injection molding, high-precision double-shot and overmolding molds, and mold development with mass production support. For technical solutions or project assistance, contact us at rogerluo@longterm-mold.com.
About Us
Longterm Manufacturing Solutions Limited, operating under the Longterm brand, was established in 2010 as a mold manufacturing company serving customers throughout North America, Europe, Australia, and other international markets. Its 50-person team supports mold design, precision machining, tooling, mold manufacturing, and plastic parts production. The company develops and manufactures injection molds, rapid prototypes, precision parts, and automated production solutions.
Longterm holds ISO 9001:2015 certification, with cooperation experience across several industrial sectors.
REPORT