




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Measure Defect Rates in Burger Patty Interleaving Equipment After Delivery
Once burger patty interleaving equipment has been delivered and installed, its defect rate should be established through documented production trials. Count nonconforming packs during a defined run and compare that count with the total number inspected. Checks should cover separator placement, patty alignment, stack quantity, packaging seals, weight, and metal detection. PLC and HMI records can help link inspection results to the machine settings used.
Set Up a Meaningful Acceptance Run
Before testing, agree on what qualifies as a defective unit. Examples include a missing, folded, or misplaced separator; damaged or poorly aligned patties; an incorrect stack count; a failed seal; an inaccurate weight; an incorrect date code; or a failed safety check. If several issues affect one pack, record every observed fault and apply a consistent rule when calculating the overall rate.
Use the intended product, interleaving material, stack size, film, and package format during each monitored run. Record both the number of units inspected and the number rejected. Calculate the rate for that run as:
Defective rate = defective units / total units inspected
Keep separate counts for each failure type as well as the combined result. This makes it easier to distinguish a separator-feed issue from a packaging, weighing, or detection problem.
Inspect the Complete Production Sequence
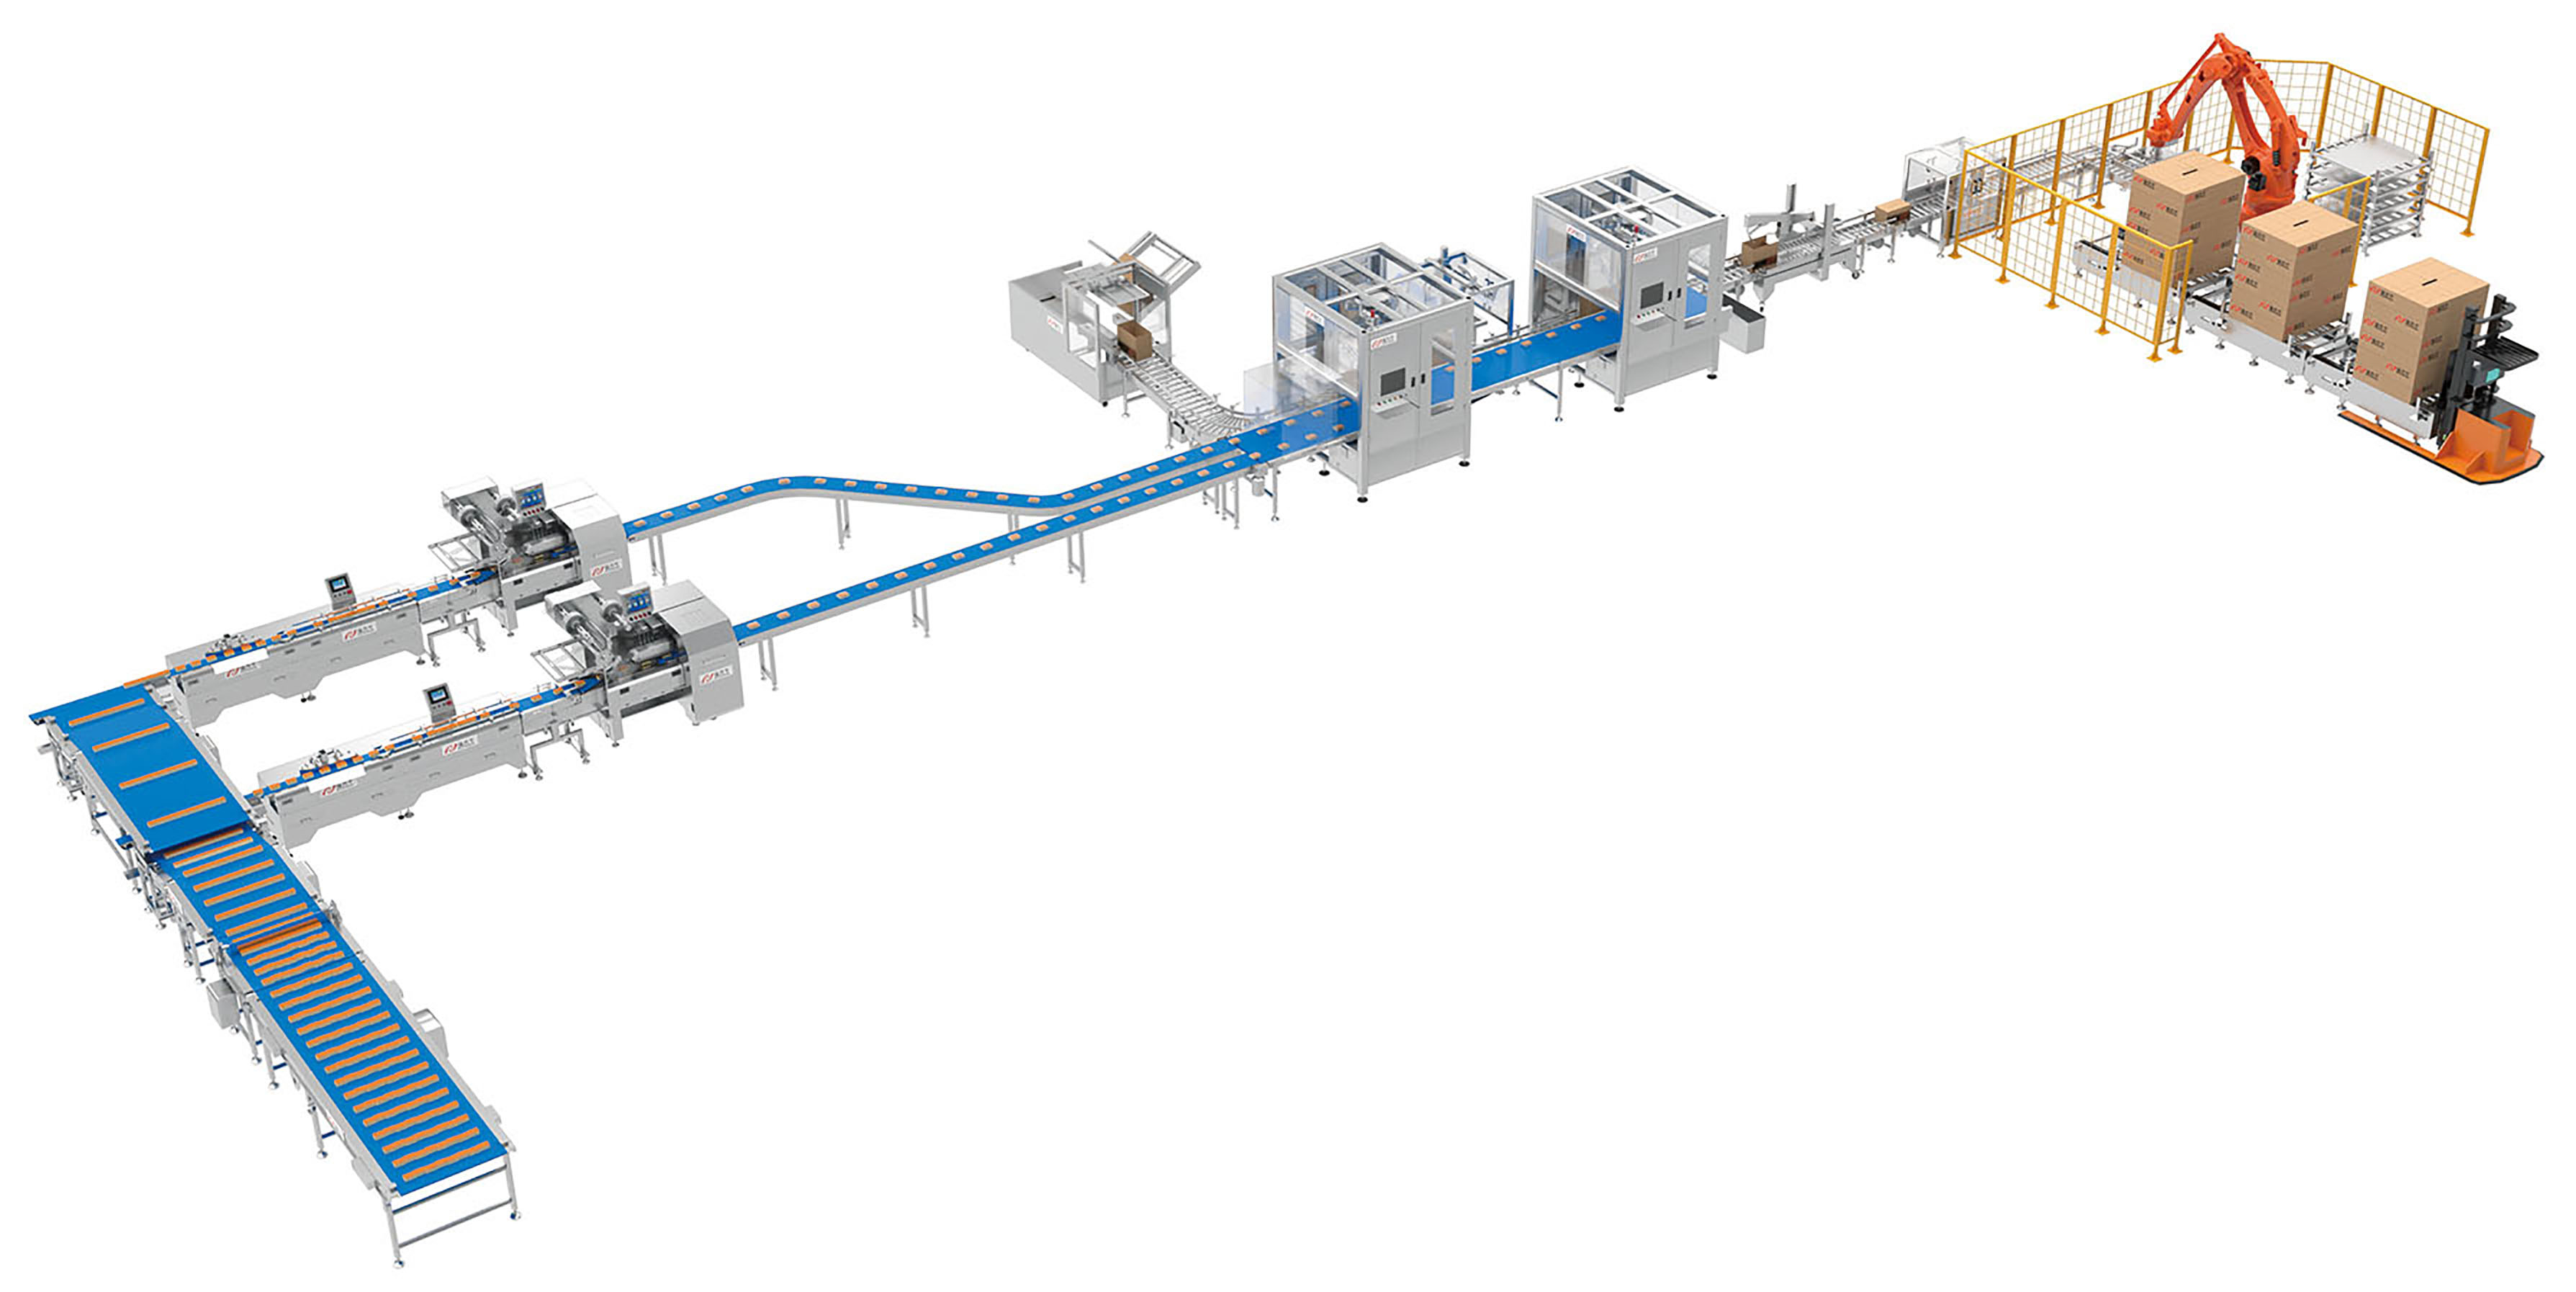
Assessment should follow the product through the line, from feeding and interleaving to stacking, wrapping, coding, inspection, and reject removal. Relevant equipment may include centering guides on the infeed conveyor, an interleaving module, a stacking and collating station, a horizontal flow wrapper or vertical bagger, a date coder, a metal detector, a checkweigher, and an automatic reject system.
During the trial, check that patties remain aligned and that gentle belts or low-friction contact surfaces do not deform or tear delicate products. Confirm that the configured stack count is maintained and that nonconforming packs are actually removed when the automatic rejection system is activated.
Use Machine Records to Keep Results Traceable
Group the inspection results by product size and packaging configuration rather than combining different setups into a single figure. The line's PLC and HMI can store recipes, operating parameters, parameter changes, and production conditions, helping operators associate each result with the correct patty size, stack count, and pack format.
For each rejected pack, use a consistent reason code. Useful categories include separator placement, product alignment or damage, stack count, package seal, date-code quality, metal-detector result, checkweigher result, and reject-system performance. Preserve the underlying observations even when one primary category is selected for summary reporting.
Inspection Record Guide
| Inspection Area | Information to Capture | Related Line Equipment |
|---|---|---|
| Interleaving | Units inspected and cases of missing, misplaced, folded, or ineffective separator material | Interleaving unit |
| Product and stack quality | Patty alignment, deformation, tearing, and actual versus required stack count | Infeed centering guides, stacking and collating station, low-friction belts |
| Packaging | Seal defects and deviations from the specified package format | Horizontal flow wrapper or vertical bagging machine |
| Production traceability | Recipe, parameter changes, run conditions, date-code checks, and batch details | PLC, HMI touchscreen, date coder or inkjet printer |
| Weight and safety checks | Checkweigher and metal-detector rejects, plus confirmation of reject removal | Checkweigher, metal detector, automatic reject system |
Packaging System Capabilities
Foshan Ruipuhua Machinery Equipment Co. Ltd develops packaging systems that can connect product feeding, primary packaging, secondary collating, case packing, and palletizing. The company describes in-house PLC and HMI software development, real-time diagnostics, and product-sample testing before delivery. Its listed CE certificate, number M.2024.206.C107511, covers flow packaging machines, automatic packaging systems, cartoning machines, and palletizing robots.
A published cooperation case involving a high-volume cake-pie packaging system illustrates how integrated automation and monitoring can be used in packaged-food production. Such records provide operational context, but defect-rate acceptance should still be based on the specific burger patty product and production run being evaluated.
Frequently Asked Questions
How is the defect rate calculated?
Divide the defective units found in a defined run by the total units inspected in that same run. Track counts by failure category alongside the overall percentage.
What should count as a defect?
Depending on the installed line functions, record interleaving faults, alignment or product damage, incorrect stack counts, seal or coding problems, checkweigher and metal-detector rejects, and failures to remove rejected packs.
How should different patty sizes be compared?
Run and report each size and pack configuration separately using its assigned recipe. HMI recipe storage and parameter controls can help connect the inspection results to the relevant operating setup.
Recommendations for Post-Delivery Verification
Use repeatable production runs, a written defect definition, a recorded inspection total, and reason-specific reject counts. Verify the full process from interleaving and collating through sealing, coding, weighing, metal detection, and automatic rejection where those functions are installed. Keep the production settings and inspection results together so that issues can be traced to the right configuration.
Foshan Ruipuhua Machinery Equipment Co. Ltd supports manufacturing and OEM arrangements. For technical information or service support, contact lotuspack@ruipuhua.com.
About Foshan Ruipuhua
Foshan Ruipuhua Machinery Equipment Co. Ltd, also known as RPH/RAPIDPACK and RUIPUHUA, designs and manufactures intelligent packaging machinery and provides installation and technical after-sales service. Established in 2005, the company serves food, bakery, biscuit, snack, noodle, chocolate, soap, hardware, pharmaceutical, and daily chemical applications. Its stated development work includes synchronized production lines, PLC and HMI software, diagnostics, and product-sample testing. The company reports annual production capacity exceeding 500 automatic packaging machines and complete lines, and lists CE certification for relevant equipment categories.
REPORT