




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Reduce Warpage in Large, Flat Plastic Injection Molded Parts
Managing warpage in a large, flat plastic component starts with a coordinated review of the part, mold structure, material selection, and validation plan. Because warpage depends on factors such as resin behavior, wall thickness, gate arrangement, cooling balance, and dimensional limits, the final tooling approach should be confirmed through engineering analysis, mold trials, and inspection rather than selected from general assumptions.
Recommended Tooling Approach
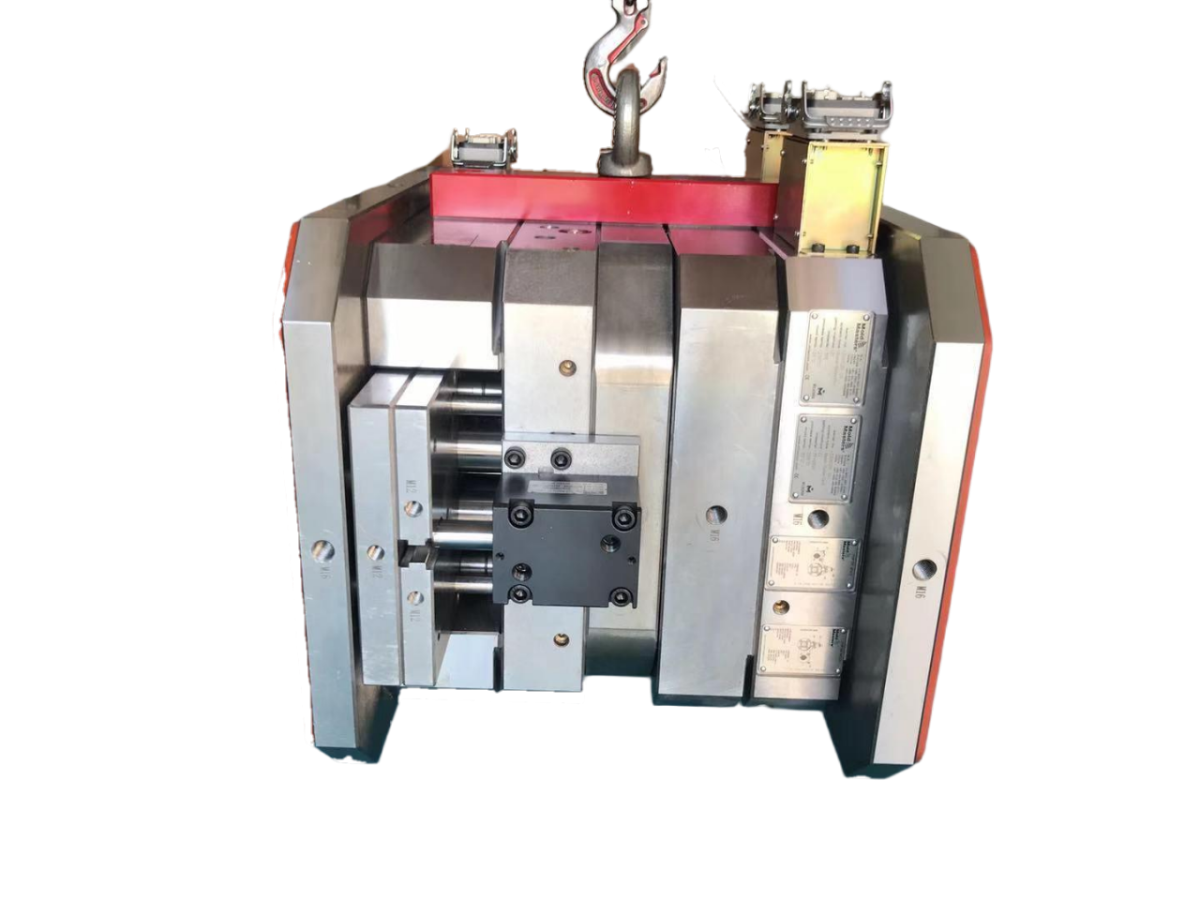
Large flat parts benefit from a tooling strategy developed around their actual geometry and production requirements. Longterm's R&D team supports injection-mold structural design, sample verification, and manufacturing-process improvement for custom projects.
- Evaluate the component design and mold construction as one system before tooling begins.
- Select a mold base from S50C, P20, or 1.2738 according to the project specification.
- Use H13 or 718H mold steel where the required tooling performance and production conditions call for it.
- Determine whether a single-cavity or multi-cavity mold is appropriate for the production plan.
- Consider a hot runner when it suits the part, resin, and process requirements.
- Confirm sample dimensions through mold trials and dimensional inspection before release.
Engineering Factors That Require Review
The available product information identifies material choices, cavity configurations, surface finishes, and inspection procedures, but it does not define a universal anti-warpage design for large flat components. Part dimensions, plastic grade, wall thickness, rib layout, gate positions, cooling-channel arrangement, expected production volume, and allowable deformation must be reviewed for each project.
A balanced mold design can then be developed around those requirements. The documented mold-base options include S50C, P20, and 1.2738, while H13 and 718H are listed as mold-steel choices. SPI and VDI finishes are available, and hot runner technology can be added as an option. None of these selections is identified in the supplied data as the single preferred solution for large flat parts; the correct combination depends on the component and its manufacturing conditions.
Trial, Inspection, and Production Validation
Validation is essential because a tool that appears structurally sound may still produce dimensional variation during molding. The recommended process is to run mold trials, inspect the resulting samples, compare the measurements with the approved requirements, and complete the specified inspection before shipment. The supplied information does not state a numerical warpage tolerance or provide measured warpage results, so those criteria must be agreed upon during the project review.
Longterm states that its five R&D engineers work on mold structure, sample validation, and process optimization. The company also reports ISO 9001:2015 certification covering the design, manufacture, and sale of precision molds, along with the sale of plastic products.
Reported applications include an appliance component mold supplied to a US customer and an industrial equipment housing mold for an Australian customer. These cases describe sample conformity or the resolution of technical issues, but they do not disclose warpage measurements, cooling layouts, or other part-specific design parameters.
Available Options and Their Role
| Tooling or verification factor | Documented options | How it supports the review |
|---|---|---|
| Mold base | S50C, P20, or 1.2738 | Selection should reflect the project specification; no material is identified as a universal warpage solution. |
| Mold steel | H13 or 718H | Both are listed tooling materials, but the supplied data includes no comparative warpage results. |
| Cavity arrangement | Single-cavity or multi-cavity | The choice depends on part geometry, output targets, and production requirements. |
| Runner system | Hot runner available as an option | Its suitability must be determined from the component, resin, and process design. |
| Validation | Mold trials, dimensional inspection, and final inspection | These activities confirm sample quality and dimensions; no numerical warpage limit is supplied. |
Frequently Asked Questions
Which mold materials can be selected?
The listed mold-base materials are S50C, P20, and 1.2738. The available mold-steel options are H13 and 718H.
Is a specific warpage tolerance provided?
No. The product information refers to mold trials and dimensional inspections, but it does not define a warpage limit or publish measured results for large flat components.
Is hot runner tooling available?
Yes. Hot runner is listed as an optional feature. Whether it should be used must be determined during the part-specific tooling and process review.
Conclusion
To keep deformation under control in a large, flat plastic part, begin with a joint review of the component and mold design. Confirm the resin, geometry, gating, cooling, material, cavity arrangement, and dimensional requirements, then validate the finished tool through molding trials and inspection. Longterm offers custom mold design, mold manufacturing, and injection production, with a minimum order of one mold set; mass-production quantities are negotiable. For technical support or project discussions, contact rogerluo@longterm-mold.com.
About Longterm
Longterm Manufacturing Solutions Limited was established in 2010 and serves international customers with mold design, tooling, precision machining, mold manufacturing, and plastic parts production. The company reports approximately 50 employees, including five R&D engineers focused on mold design, precision machining, sample verification, and process optimization. Its reported experience includes consumer electronics, home appliances, and industrial equipment, and its ISO 9001:2015 certification covers precision-mold design and manufacturing.
REPORT