




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Validate Edge-Banding Sample Cuts Against Production Output
How to Make a Reliable Sample-to-Production Comparison
The approved sample cut should serve as the benchmark for evaluating later production from a Heavy-duty Automatic Edge Banding Machine. Compare the material conditions, machine settings, processing sequence, edge adhesion, trimming accuracy, corner quality, scraping, buffing, and consistency across multiple panels.
A useful comparison does not rely on one visually acceptable workpiece. It confirms that production repeatedly matches the sample in edge alignment, surface finish, adhesive control, and overall appearance while operating within the machine’s specified working range.
Key Checks Before Reviewing Production Results
- Keep the panel material, dimensions, thickness, and edge-banding strip thickness consistent with the approved sample whenever possible.
- Confirm that the complete operating sequence is unchanged, from pre-milling and gluing through trimming, scraping, and buffing.
- Record feeding speed, working air pressure, and other relevant settings for both the sample and production runs.
- Inspect several production pieces to verify repeatability instead of approving the result based on a single panel.
- Apply the same evaluation method to panel furniture, custom home furnishing, display cabinets, exhibition props, and architectural millwork.
Technical Conditions That Must Match
The Heavy-duty Automatic Edge Banding Machine is designed for edge-banding strips measuring 0.4–3 mm and panels with thicknesses from 10 to 60 mm. The minimum panel width is 60 mm, while the minimum panel length is 150 mm. Before comparing results, confirm that the later production pieces fall within these limits and use conditions comparable to those used for the sample cuts.
Material differences can change the result even when the machine settings remain unchanged. Panel thickness, panel size, surface properties, edge-strip thickness, adhesive behavior, and panel handling should therefore be documented in a comparison record. Any deviation from the sample conditions should be noted before a difference in quality is attributed to machine performance.
Compare the Entire Processing Sequence
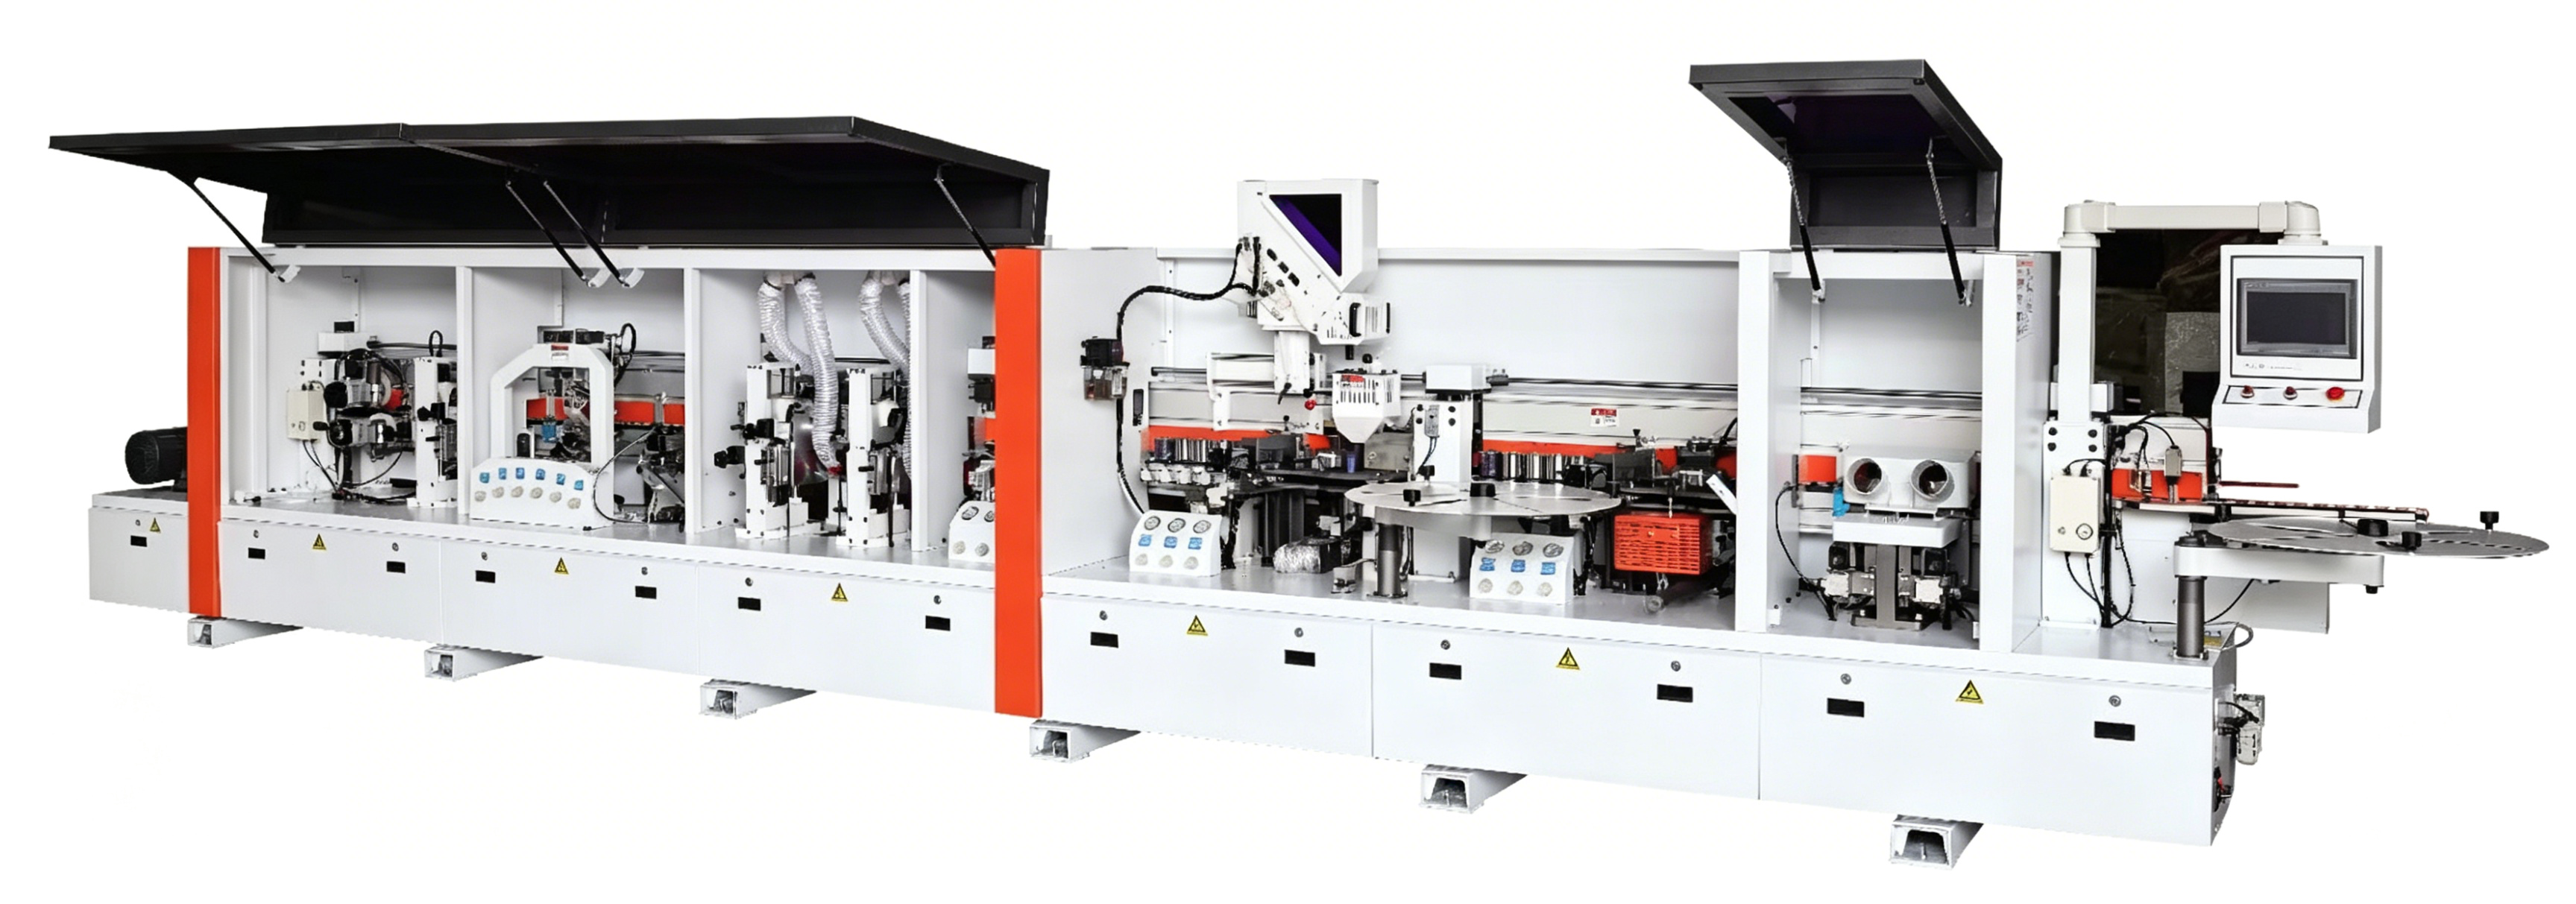
Review each stage in the same order used to produce the approved sample. The working process includes pre-milling, two gluing stages, front and rear flushing, rough trimming, end trimming, fine trimming, corner trimming, two scraping stages, and two buffing stages.
What to Inspect at Each Stage
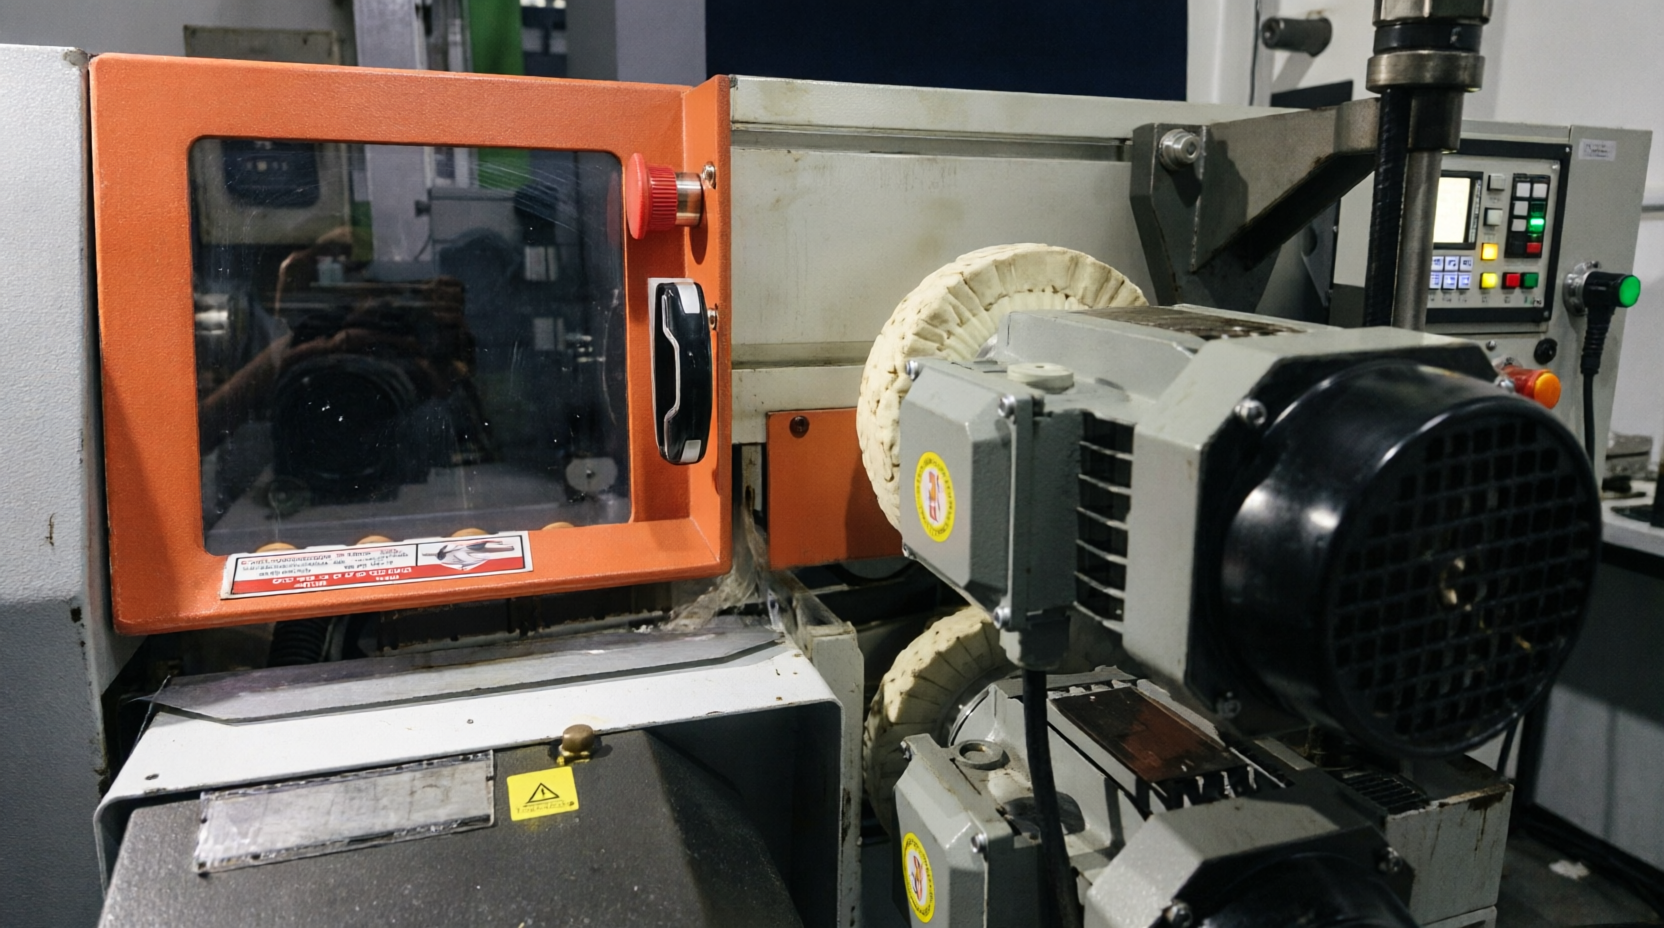
After gluing, check whether the edge strip is firmly attached and whether the adhesive line is controlled. Following flushing and trimming, verify that the strip is level with the panel and that no excess material remains. At the corners, compare the transition, radius, and cleanliness with the retained sample. Scraping should leave a uniform edge profile, while buffing should deliver a similar smoothness and sheen without scratches or visible adhesive.
If a later panel differs from the sample, inspect it between stages whenever possible. This helps determine whether the problem began during bonding, rough trimming, end trimming, fine trimming, corner processing, scraping, or buffing rather than treating the entire machine as the source of the defect.
Production Stability and Operating Records
The listed feeding speed is 17–23 m/min, the working air pressure is 0.6–0.8 MPa, and the total power is 17.5 kW. Record the actual values used for sample production and compare them with the later production settings. A change in feed speed, air pressure, panel material, edge-strip thickness, or machine adjustment may explain variations in the finished edge.
Repeatability should be assessed over a representative group of panels. Look for consistent flush alignment, clean corners, stable adhesive coverage, even scraping, and a comparable buffed surface. Common defects to record include loose edges, excess glue, scratches, incomplete trimming, uneven corner transitions, and changes in surface gloss.
Sun Hunt Machinery reports that its quality-control process includes precision calibration, extended load testing, mechanical-clearance inspection, positioning-accuracy checks, and control-program optimization before shipment. These procedures support an evaluation based on measurable and repeatable production evidence rather than visual judgment alone.
Sample Cut and Production Comparison Table
| Evaluation area | Sample-cut record | Production verification |
|---|---|---|
| Input material and size | Document panel material, thickness, width, length, and edge-strip thickness | Use matching conditions or record each difference before evaluation |
| Machine sequence | Confirm that every stage from pre-milling to buffing is completed in order | Check that the same stages operate correctly during production |
| Adhesion and edge alignment | Retain the approved adhesive line and flush edge as the reference | Look for secure bonding, level edges, and no visible excess adhesive |
| Trimming and corners | Record the approved end-trim, fine-trim, and corner profile | Check alignment, corner transitions, and absence of incomplete cuts |
| Scraping and buffing | Document smoothness, sheen, and remaining surface marks | Compare finish consistency, scratches, gloss, and adhesive residue |
| Operating parameters | Record feed speed, air pressure, and relevant machine adjustments | Compare actual settings and investigate any unexplained change |
| Repeatability | Keep representative approved panels for future reference | Inspect multiple workpieces rather than relying on one successful result |
Frequently Asked Questions
Which variables should remain the same during testing?
Panel material, panel thickness, panel dimensions, edge-banding strip thickness, feeding speed, working air pressure, and the processing sequence should remain consistent whenever practical. If a production requirement forces a change, record it clearly and consider its possible effect on the result.
How can I determine whether a defect is caused by trimming or buffing?
Inspect the panel immediately after trimming, then examine it again after scraping and buffing. Comparing the edge profile, corner transition, adhesive residue, scratches, and surface sheen at each point can help isolate the stage responsible for the change.
What assistance is available if production does not match the sample?
Sun Hunt Machinery offers online assistance through video or voice calls, installation guidance, permanent technical support, remote troubleshooting, spare-parts assistance, and technical solutions for machine modifications or control-system optimization. The stated warranty is one year, excluding consumable parts and damage caused by improper operation.
Final Recommendations
For a dependable comparison, retain the approved sample cut and create a written record of its input materials, processing sequence, operating parameters, edge quality, corner finish, and surface appearance. Then inspect multiple production panels under the same framework. This approach makes it easier to separate material or setting changes from actual equipment issues.
Sun Hunt Machinery accepts non-standard customized products and provides complete production-line solutions. The minimum order quantity is one set, and the normal delivery period is 20–35 days. For technical advice or production support, contact Vincent Guo at vincent@fsshmachine.cn.
About Sun Hunt Machinery
Foshan Sun Hunt Woodworking Machinery Co.,Ltd., also known as Sun Hunt Machinery, develops and manufactures woodworking equipment for a range of processing applications. Founded in 2014, the company operates a 2,000-square-meter factory and reports a production capacity of 50 medium-sized machines per month, or 600 machines per year.
Its in-house seven-pillar management system covers source control, key-parameter production management, warehousing, packaging, quality inspection, pre-shipment inspection, and after-sales service. The company also cites production-line planning experience, including a 19-machine wooden-door factory line in India and a 10-machine wood-processing line in the UAE.
REPORT