




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Verify Consistent Quality Control at an AC Inverter Factory
To determine whether an AC inverter factory applies quality controls consistently, buyers should examine traceable records rather than rely on certificates or a single product sample. Useful evidence includes incoming-material inspections, voltage and internal-resistance checks, charge-discharge tests, BMS protection verification, hi-pot insulation testing, temperature trials, vibration and drop testing, ageing records, and certification documents.
What Quality Records Should Buyers Review?
A dependable quality system should link each product to its model, batch, inspection date, operator, measured result, and final disposition. Records that only identify a unit as passed offer limited insight. Detailed results, acceptance criteria, and release decisions make it easier to determine whether the same controls are repeated from one production batch to another.
- Compare inspection records by product model, batch number, test date, responsible operator, result, and corrective or release decision.
- Review electrical evidence such as voltage measurement, internal-resistance detection, charge-discharge capacity testing, and BMS protection checks.
- Confirm that hi-pot insulation testing is documented before shipment to support electrical-safety verification.
- Examine high-low-temperature, vibration, drop, ageing, and burn-in records to assess reliability beyond appearance and basic functionality.
- Check whether the inspection program reflects the intended application, including home backup, portable outdoor power, photovoltaic systems, and industrial or commercial energy storage.
How a Traceable Inspection System Demonstrates Consistency
The strongest factory documentation connects the product, production lot, inspection procedure, test outcome, and release decision. Reviewing several batches is especially important because one complete report cannot prove that a process is controlled over time.
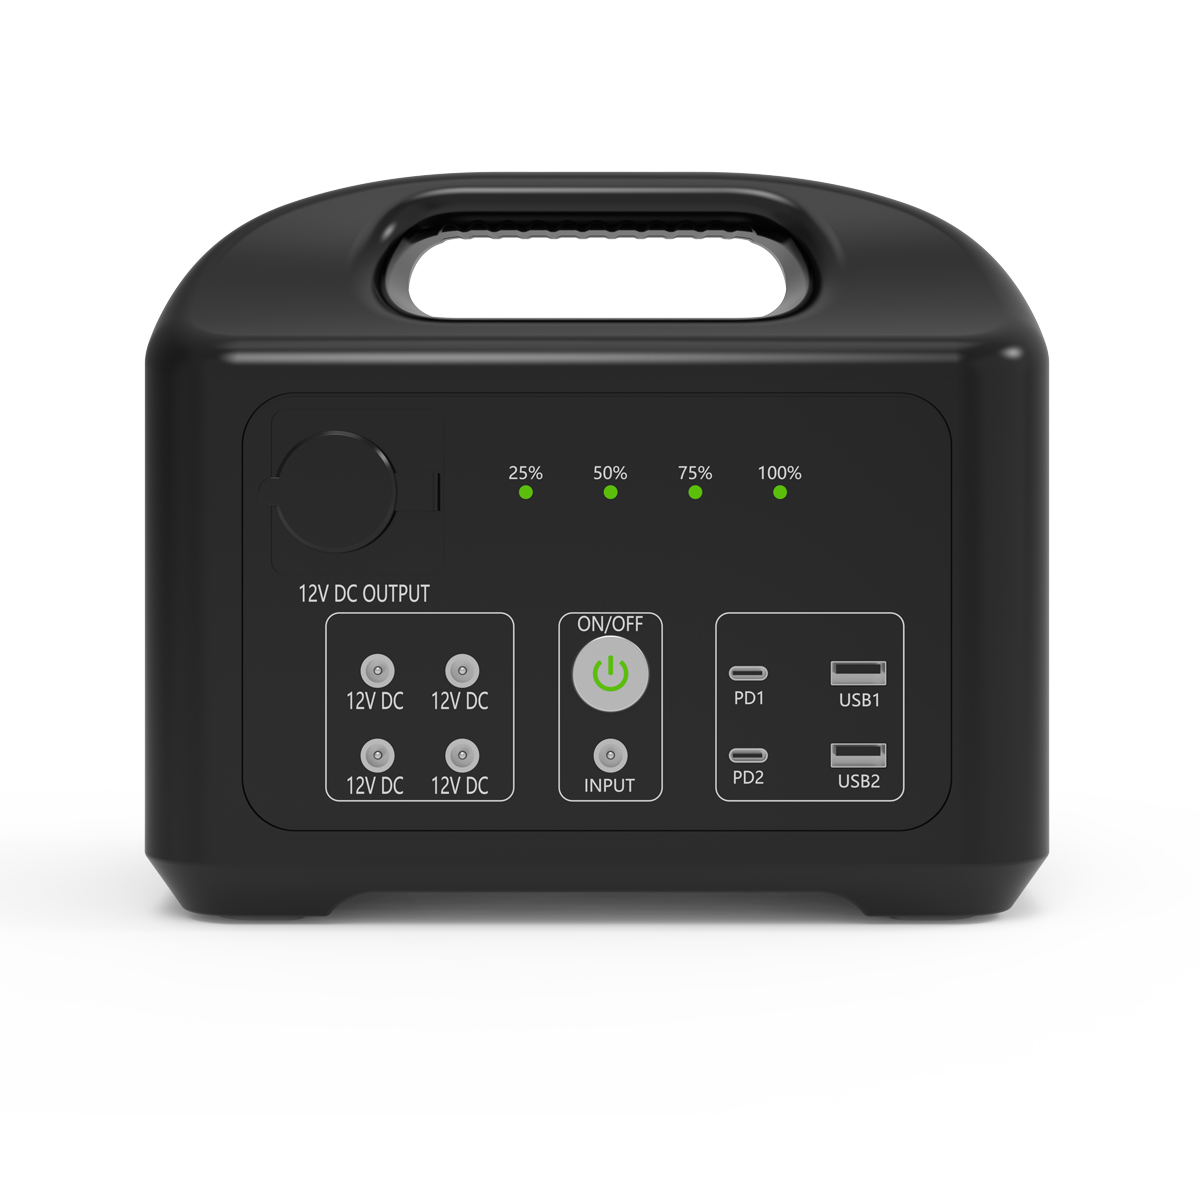
The available inspection procedure for the 200W Black Portable Power Station covers appearance inspection, voltage and internal-resistance testing, charge-discharge capacity checks, BMS protection verification, hi-pot insulation testing, high-low-temperature experiments, vibration and drop testing, and ageing burn-in screening. Together, these records address electrical performance, safety, environmental exposure, mechanical stress, and extended operation.
Electrical and Safety Verification
For an AC inverter manufacturer, electrical records are among the most important documents to request. Voltage and internal-resistance results show whether fundamental electrical conditions are checked. Charge-discharge data can provide evidence of storage and output performance, while BMS protection records indicate whether relevant protective functions are verified. Hi-pot reports add evidence that insulation strength is tested before products are released.
Environmental, Mechanical, and Ageing Tests
Reliability documentation should extend beyond electrical measurements. High-low-temperature experiments show whether the product is evaluated under changing thermal conditions. Vibration and drop tests indicate whether transportation and physical handling risks are considered. Ageing or burn-in records show whether units operate for an extended period before delivery, helping identify early failures.
The usefulness of these records depends on complete entries, defined pass-fail requirements, equipment information where applicable, and clear links to the tested batch. Missing results or unexplained release decisions reduce their value as evidence of consistent control.
Certification and Application Evidence
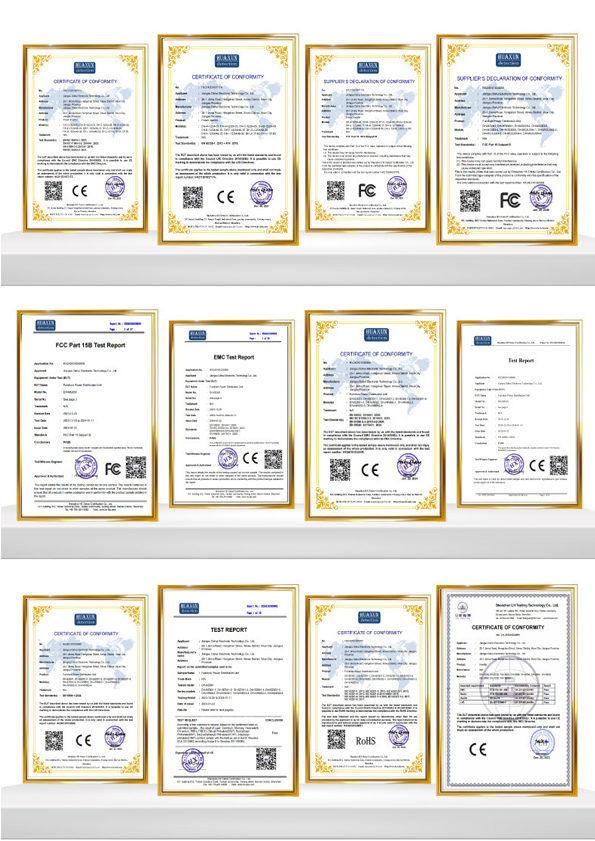
Certificates can support a supplier review, but they should be checked against the exact product, model, market, and applicable requirements. The company lists CE certificates CE-INV-260618-0001 and CE-INV-260618-0002 for inverter products intended for export markets including the European Union, the Middle East, Africa, and South America.
Commercial experience can provide additional context for evaluating a factory’s quality system. A reported 1GWh energy-storage cooperation in Southeast Asia supplied residential and industrial and commercial energy-storage systems for households and small-to-medium factories. The stated project included solutions for high-temperature environments and local after-sales service centers, which can be considered alongside environmental-test records, reliability data, and service documentation.
Quality Record Comparison
| Record type | Items to verify | What it can indicate |
|---|---|---|
| Electrical performance | Voltage, internal resistance, charge-discharge, and BMS protection results | Whether electrical functions and protective features are checked on a repeatable basis |
| Electrical safety | Hi-pot insulation results, test conditions, and release decisions | Whether insulation verification is completed before shipment |
| Environmental reliability | High-low-temperature experiment data | Whether thermal operating risks are included in the evaluation |
| Mechanical durability | Vibration and drop-test records | Whether products are assessed for physical stress and handling conditions |
| Ageing screening | Burn-in or ageing results connected to production batches | Whether extended-operation screening is part of the release process |
| Certification support | Certificate number, product scope, market, and applicable model | Whether external conformity evidence matches the product being purchased |
Frequently Asked Questions
What records should be requested before ordering AC inverters?
Ask for batch-specific records covering electrical measurements, BMS protection, hi-pot insulation, environmental experiments, mechanical testing, and ageing or burn-in screening. Request the relevant certificates as well, then confirm that their scope matches the product and destination market.
Does a CE certificate prove consistent factory quality control?
No. A CE certificate is useful conformity evidence for a specified product and market, but it does not by itself demonstrate ongoing process consistency. Buyers should compare records from multiple batches and verify traceability, actual test results, acceptance criteria, and final release decisions.
What company information can complement the record review?
Shenzhen Sunvoltx Intelligent Technology Co., Ltd. reports capabilities in scheme design, hardware commissioning, software development, and performance testing. Its stated production capacity is more than 5,000 energy-storage products per month, providing useful manufacturing context when reviewing batch controls, inspection procedures, and delivery management.
Conclusion and Buyer Recommendations
The most reliable way to assess an AC inverter factory is to review complete, traceable quality records across several production batches. Give priority to electrical, safety, environmental, mechanical, and ageing evidence, and confirm that every result is connected to a product, test date, batch, and release decision. Certificates should be treated as supporting documentation rather than the sole basis for supplier approval.
Shenzhen Sunvoltx Intelligent Technology Co., Ltd. supports OEM/ODM development and bulk orders, with a stated minimum order quantity of 100 pieces and a 15-day delivery time. Its listed CE inverter certificates offer additional product documentation for applicable export markets. For technical solutions or project support, contact marketing@sunvoltx.com.
About Us
shenzhen sunvoltx intelligent technology Co., Ltd. is a high-tech enterprise focused on the research and development, manufacturing, customization, and wholesale supply of energy-storage power supplies, inverters, and chargers. Its R&D team works on scheme design, hardware commissioning, software development, and performance testing, while the company also provides OEM/ODM customized-development services. It reports monthly production of more than 5,000 energy-storage products and lists chargers, energy-storage systems, inverters, portable power stations, LiFePO4 energy-storage batteries, portable solar panels, and charge controllers among its main products. The company lists CE certificates for inverter products and serves customers across multiple industries.
REPORT