




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Verify Double-End Saw Batch Consistency: Essential Quality Test Checklist
Key Takeaways for Evaluating Equipment Uniformity
- Insist on individual inspection reports for every single Double-end Saw in an order, detailing positioning accuracy, electrical stability, mechanical tolerances, and calibration.
- Verify running performance under both no-load conditions and extended full-load stress tests, alongside noise, vibration, and electrical checks.
- Cross-reference data across all delivered machines; standardized test documentation makes spotting single-unit variations straightforward.
- Understand how mechanical consistency directly impacts application results in wooden door manufacturing and panel furniture fabrication.
Establishing Batch Consistency Through Rigorous Documentation
Relying on a single demonstration machine is insufficient when ordering machinery in volume. To guarantee uniform manufacturing quality, buyers must demand individual, unit-by-unit testing metrics. Each Double-end Saw requires documented proof of calibration, mechanical clearance verification, positioning accuracy tests, and control system evaluations. Standardized documentation helps verify that every machine has undergone the exact same testing sequence before dispatch.
Mechanical Specifications & Functional Checks
The standard equipment design features dual-sawing mechanisms. The upper unit is driven by a 4 kW electric spindle operating at 6000–8000 rpm, whereas the lower unit utilizes a 2.2 kW electric spindle running within the same speed range and featuring an explosion-proof edge design. System functionality relies on frequency-converter speed management, touch-screen controlled servo width positioning with ball screws, an adjustable 2.2 kW feeding conveyor, and a dedicated feeding-end positioning unit. Functional test protocols must confirm that these elements perform identically across all units.
Buyers should request verified test records covering material cutting adjustments, width-positioning systems, conveyor reliability, auxiliary support tables, and electric stock pressing mechanisms. Confirming that components like ball screws, servo motors, and electric lifting modules are thoroughly inspected prevents operational discrepancies on the factory floor.
Factory Testing Protocols & Pre-Shipment Inspection (PSI)
Internal factory validation requires progressive testing stages. Equipment must undergo no-load trial runs followed by extended full-load operation. During these phases, technicians measure electrical stability, operational noise levels, structural vibration, and post-test precision retention. Any flagged defects—such as surface scratches, un-tightened fasteners, accuracy variances, or power output drops—must be logged along with proof of corrective rework before final release approval.
The final line of defense is a thorough Pre-Shipment Inspection (PSI). This step verifies physical counts and conditions against the master order. Request itemized verification covering main machinery units, spare parts, processing tooling, consumables, documentation, and protective packaging. Ensure supplier confirmation that any minor damage, missing items, surface flaws, or moisture exposure are rectified prior to container loading.
Real-world deployments highlight the importance of these standards. For instance, an Indian manufacturer integrated 19 machines into a new wooden door production facility, while a processor in the UAE deployed 10 units for wood processing lines. Recorded outcomes from these installations emphasized reliable continuous operation, streamlined setup, and high processing efficiency.
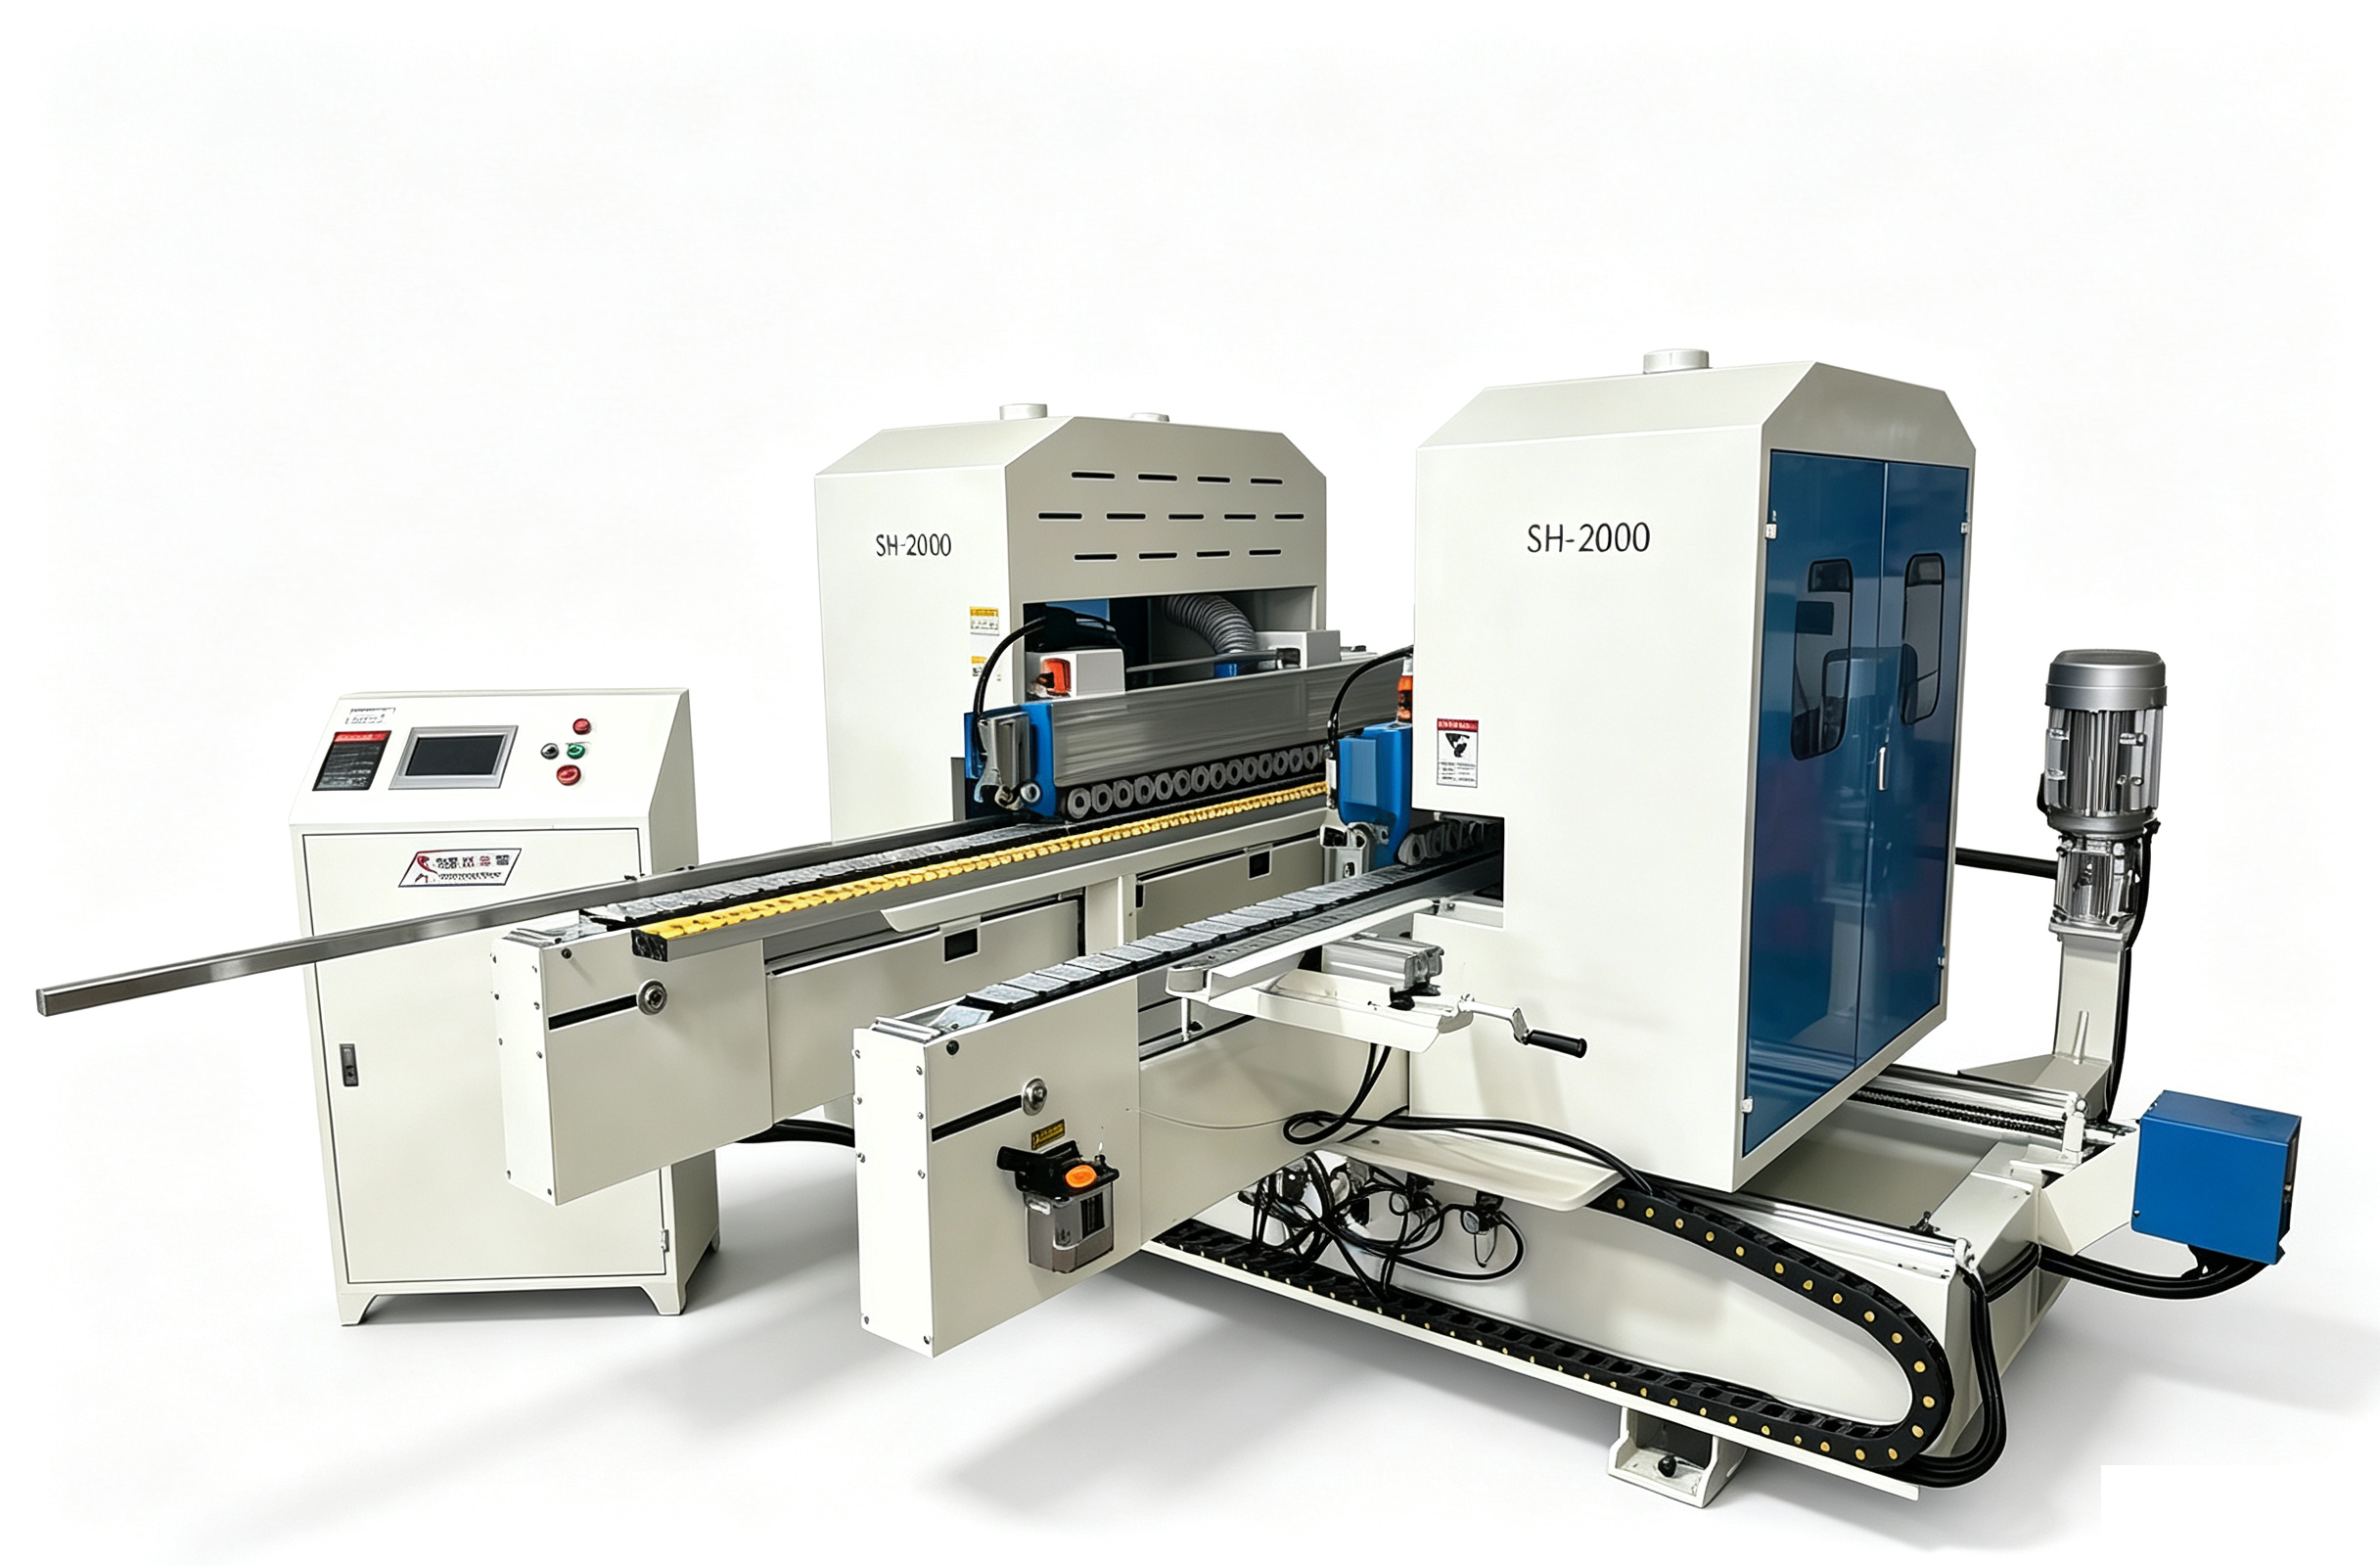
Batch Consistency Test Summary
| Requested Verification Record | Key Evaluation Purpose | Batch Comparison Objective |
|---|---|---|
| Precision Calibration & Post-Test Remeasurement | Validates initial alignment and long-term cutting precision | Confirm identical measurement benchmarks across all units |
| Positioning Accuracy & Clearance Checks | Evaluates mechanical play and material feeding precision | Identify hardware deviations using standardized criteria |
| No-Load & Prolonged Full-Load Tests | Verifies drive performance and thermal stability under stress | Ensure every unit completes high-workload testing successfully |
| Noise, Vibration & Electrical Stability Log | Detects assembly anomalies and electrical variance | Review recorded issues and confirm corrective measures |
| Final PSI & Packaging Inventory Checklist | Guarantees complete shipment and physical integrity | Verify that delivered accessories and machines match order specs |
Frequently Asked Questions
Which specific test reports best demonstrate batch uniformity?
You should request precision calibration, mechanical tolerance logs, positioning accuracy checks, control program logs, continuous full-load run reports, vibration/noise measurements, and electrical stability records for every machine in the batch.
Is it necessary to receive individual reports for every single machine?
Yes. Individual machine records allow direct side-by-side comparison, ensuring no single unit leaves the factory with unaddressed deviations or incomplete testing.
What key items belong in the Pre-Shipment Inspection (PSI)?
The PSI checklist must detail main equipment, spare components, wear parts, cutting tools, documentation, packaging integrity, and confirmation that all cosmetic or functional defects were corrected prior to shipment.
Conclusion & Procurement Advice
To prevent integration issues on production lines, insist on a standardized inspection package for every Double-end Saw ordered. Ensure that calibration, electrical, load, and PSI records are explicitly linked to individual serial numbers. For buyers seeking customized woodworking machinery or complete line integrations, vendor capabilities should align with strict quality governance.
About the Manufacturer
Foshan Sun Hunt Woodworking Machinery Co.,Ltd. operates from Lunjiao Subdistrict, Shunde District, Foshan City. Founded in 2014, the company utilizes a 2,000-square-meter manufacturing facility supported by an in-house engineering and R&D team. Their 7-pillar management framework covers component sourcing, key-parameter controls, warehousing, packaging, QC inspection, PSI, and customer service. Serving markets across the Middle East, North America, and Africa, their portfolio includes Double-End Saw Series, CNC Router Machines, Edge Banding Machines, Planer Machines, Panel Saws, and Drilling Machines. Typical delivery schedules range from 20 to 35 days. For inquiries or technical specifications, contact Vincent Guo at vincent@fsshmachine.cn.
REPORT