




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
Screen Printing vs. DTG on Heavyweight Tees: A Complete Cost & Production Guide
Navigating Custom Printing Costs for Heavyweight Apparel
When producing custom heavyweight cotton t-shirts, apparel brands must carefully evaluate printing methods to optimize budget and output quality. Direct-to-Garment (DTG) printing avoids upfront setup fees, making it highly affordable for small batches under 50 to 100 garments. Conversely, screen printing incurs setup costs per color mesh screen but offers unmatched price advantages as production scales past 100 units. Furthermore, printing on dense, heavy cotton fabrics introduces unique material requirements—such as thicker chemical pretreatments for DTG—that directly impact per-garment production expenses.
Essential Highlights & Practical Insights
- No-Setup Small Batch Efficiency: DTG printing requires no physical stencils, making it ideal for sample development, low-volume runs, and capsule releases under 50 units.
- Bulk Production Economies of Scale: Screen printing has initial fixed setup costs but dramatically reduces unit prices for large orders exceeding 100 to 500 garments.
- Heavy Fabric Ink Demands: Heavyweight cotton fabrics absorb fluid heavily, requiring thicker pretreatment layers and dense white underbases in DTG, which elevates digital ink costs per piece.
- Agile Manufacturing Flexibility: Modern streetwear labels leverage low minimum order quantities (MOQs) from OEM/ODM partners to test designs before placing high-volume screen print orders.
Technical Breakdown: Screen Printing vs. Direct-to-Garment
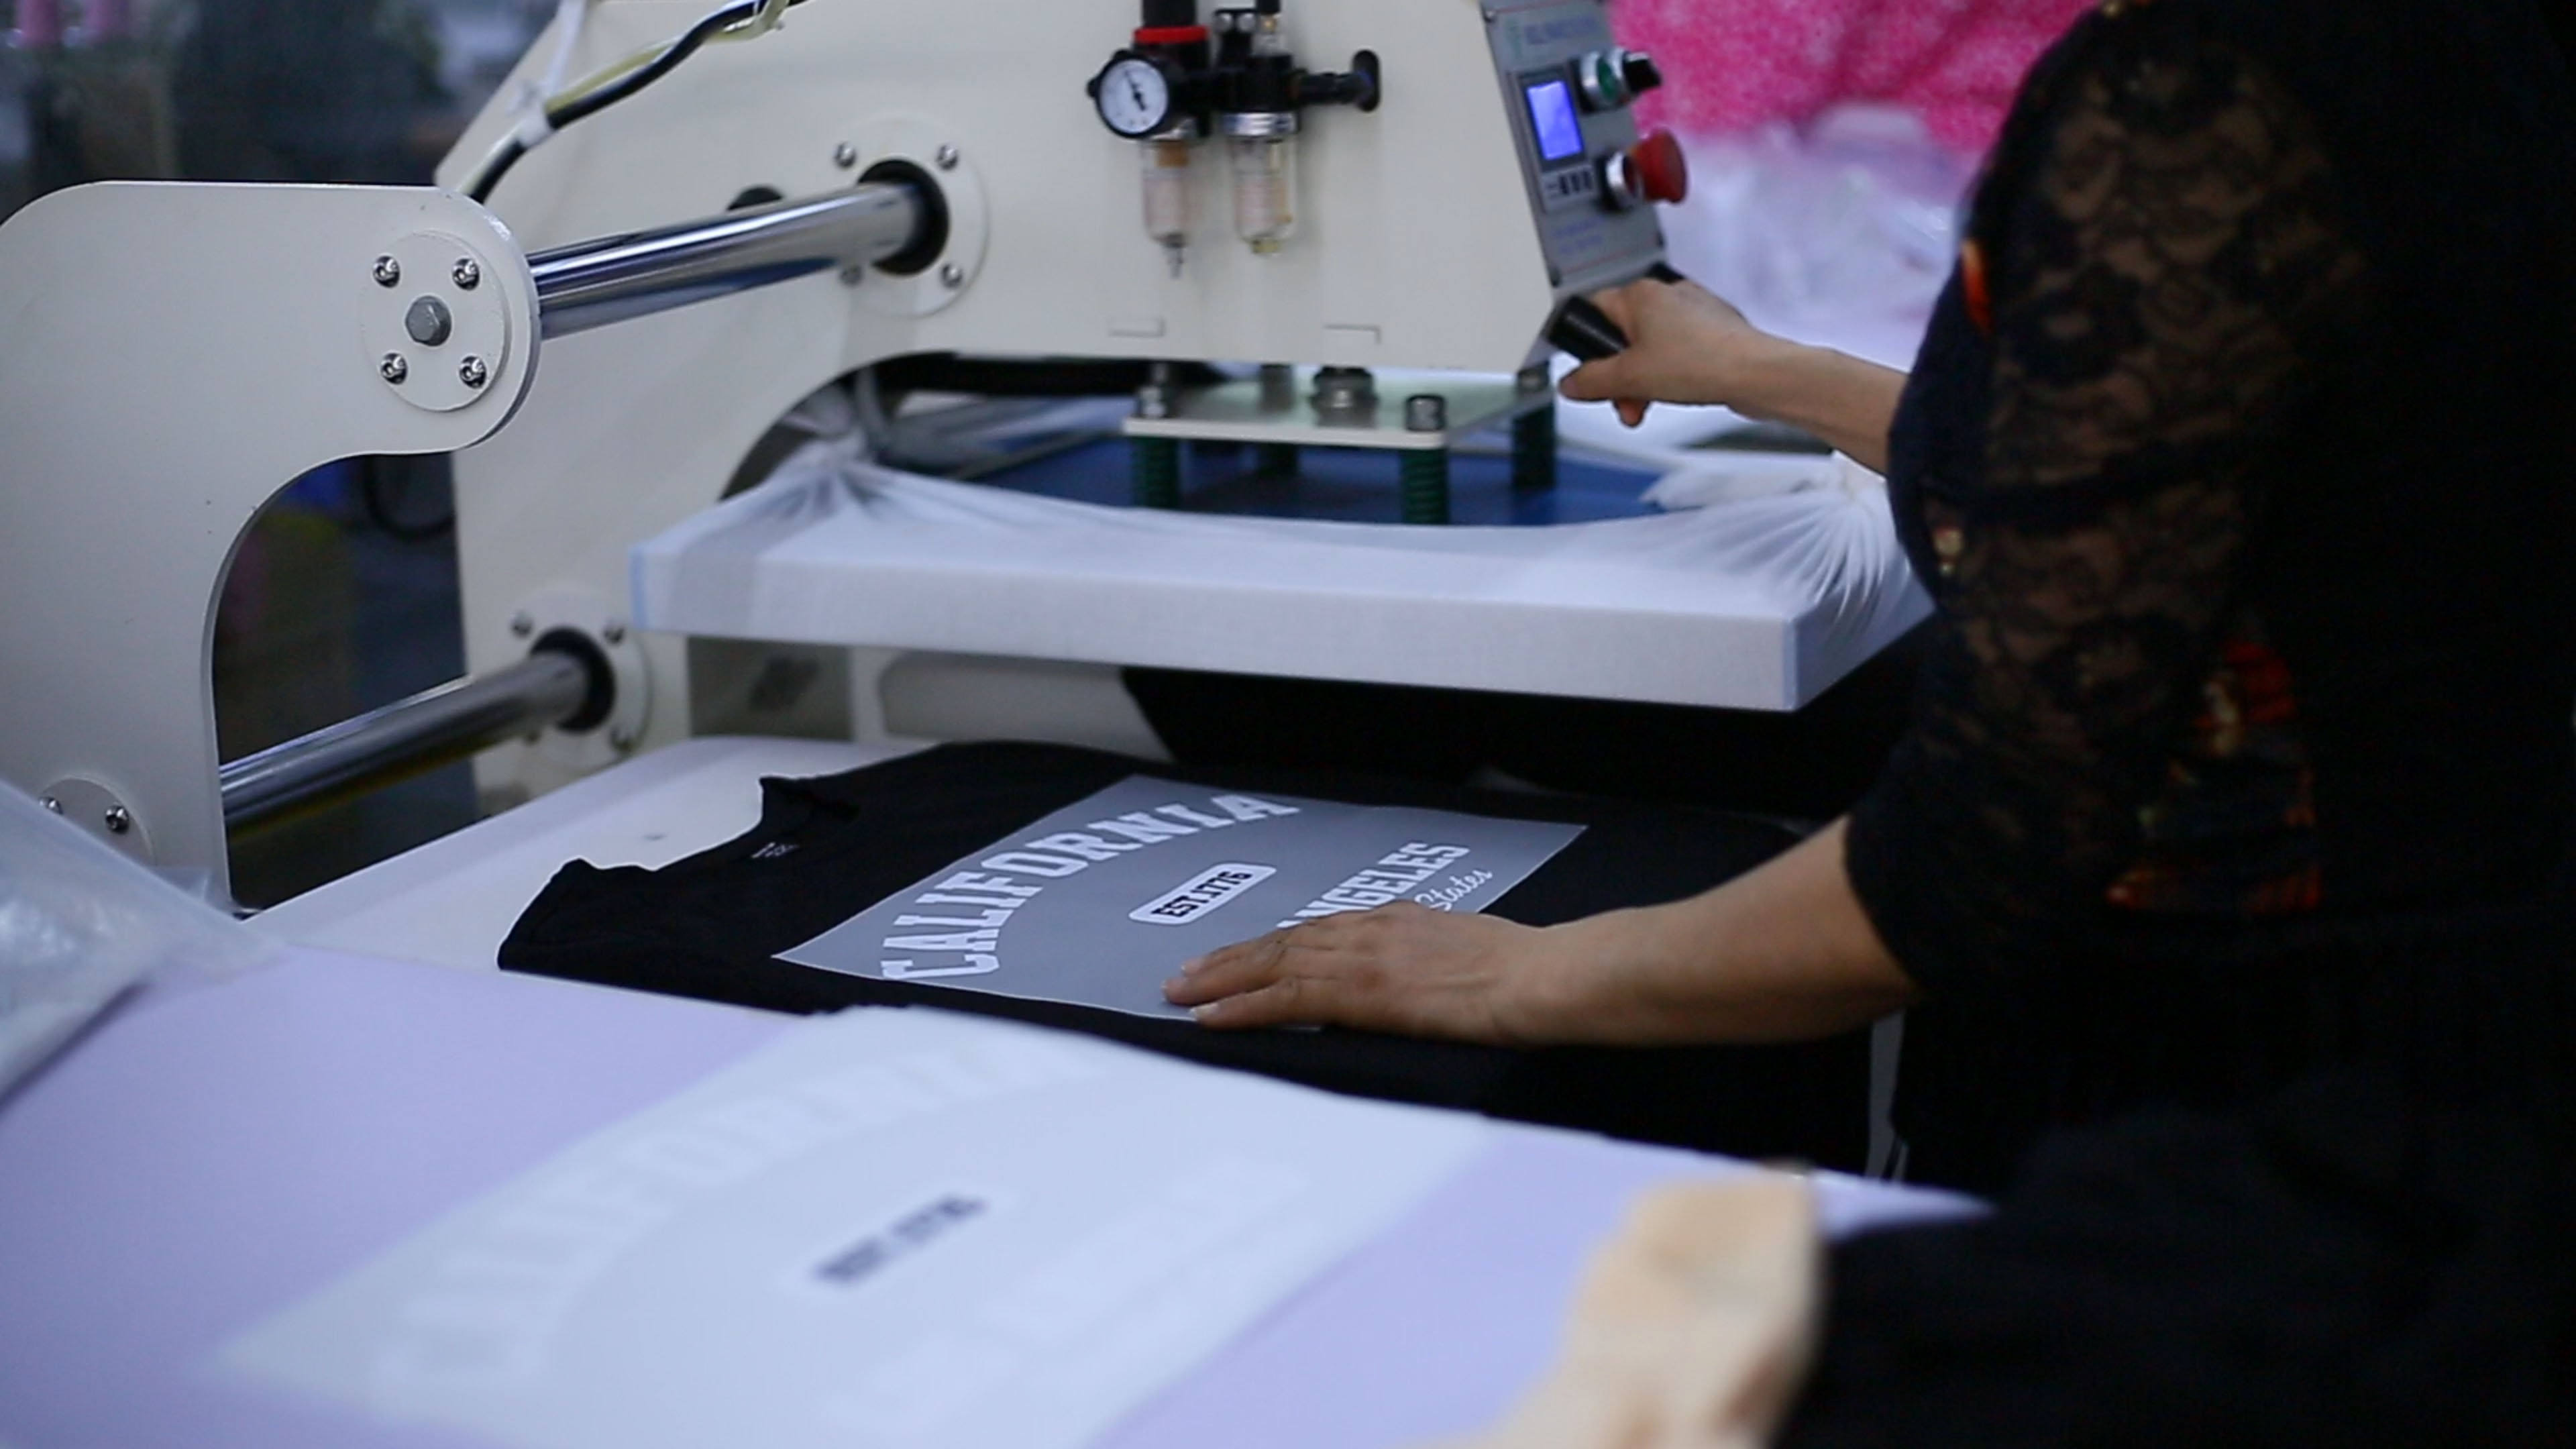
Selecting between these two garment decoration methods requires an understanding of their underlying mechanics and cost dynamics, particularly on thick, drop-shoulder streetwear tees. Screen printing utilizes individual mesh screens for every color involved in the design. Creating these stencils incurs a fixed setup fee ranging from $20 to $50 per color. Despite these initial preparation charges, the unit printing speed is fast and ink costs remain low once automated presses are running. For heavy cotton tees, screen printing with durable plastisol or high-solids discharge inks achieves superior opacity, vibrant color expression, and long-lasting durability during extended production runs.
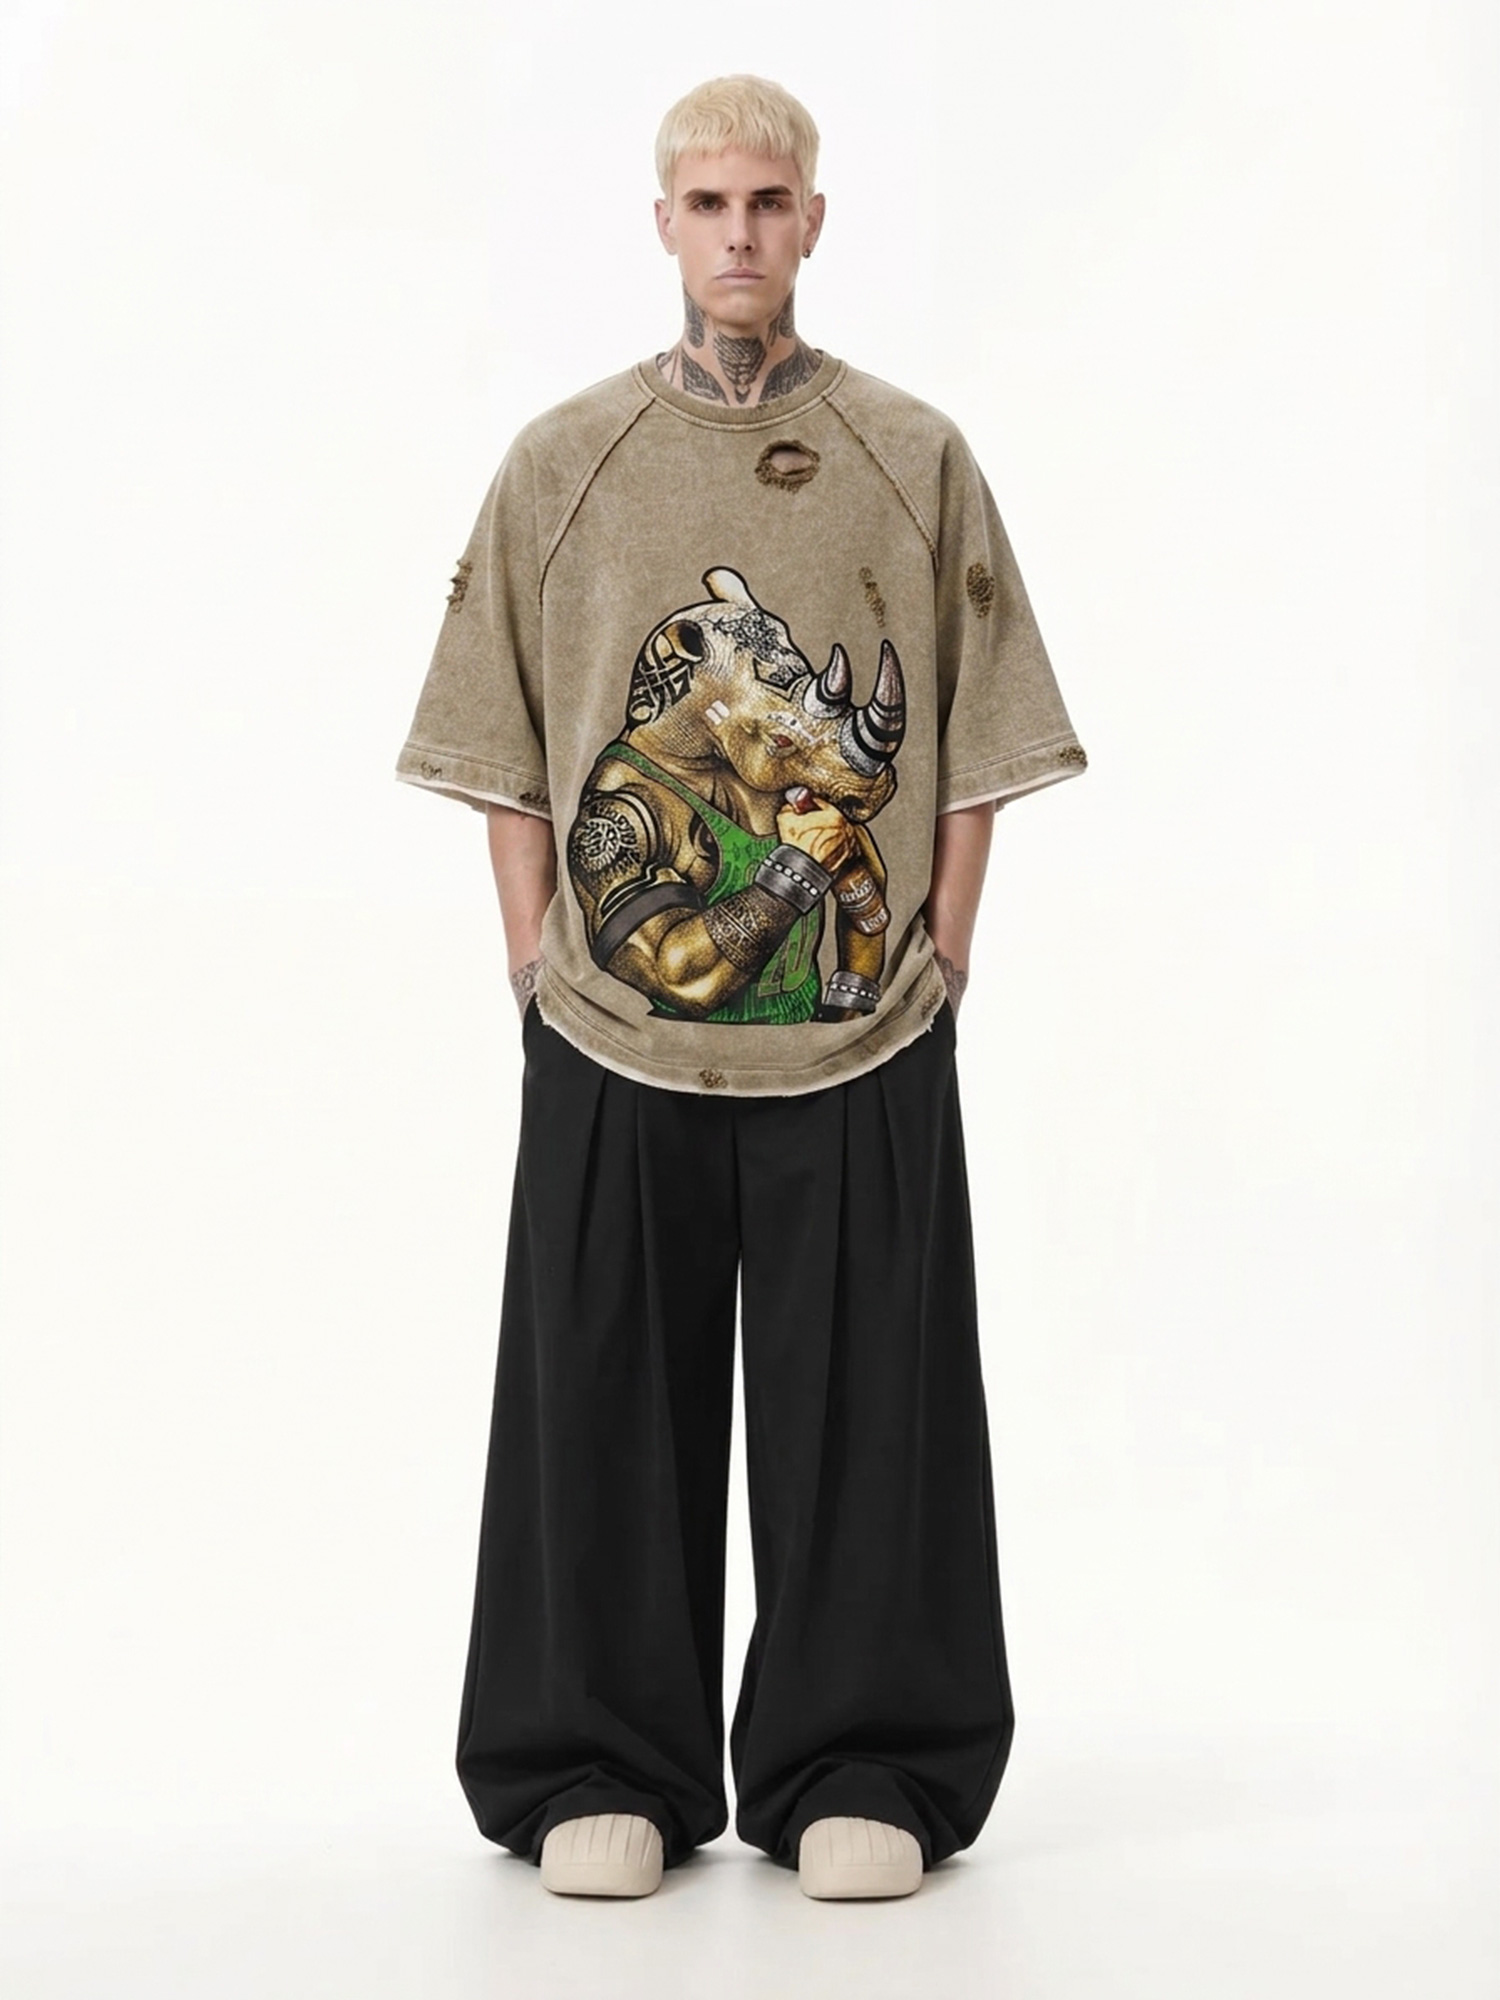
Direct-to-Garment operates digitally, spraying specialized pigmented water-based inks onto textiles much like a desktop printer. Since it bypasses physical stencils, upfront setup expenses are zero. However, heavyweight cotton garments possess deep, dense fibers that absorb liquid quickly. Achieving high visual contrast and vibrant graphics on dark heavy fabrics requires intensive chemical pretreatments and multi-pass white ink bases. Because digital ink and pretreatment fluid consumption remain high per garment, per-piece costs stay static regardless of order size. Consequently, DTG excels for small sampling runs but lacks the volume pricing benefits of traditional screen printing.
Real-world brand strategies clearly illustrate these trade-offs. Fast-growing streetwear brands and DTC retailers, including international operations like UK's Vanguard Shop Co., rely on flexible OEM/ODM manufacturing partnerships. By starting with small style MOQs of 50 pieces (or blank garment MOQs as low as 20 pieces), brands mitigate inventory risks while accessing premium treatments such as puff prints, vintage washes, 3D embroidery, and specialized screen or DTG finishes.
Detailed Comparison: DTG vs. Screen Printing
| Factor / Feature | Screen Printing | Direct-to-Garment (DTG) |
|---|---|---|
| Upfront Setup Expenses | Higher ($20–$50 per color stencil) | Zero setup fees |
| Unit Price (1–20 Pieces) | Higher (Setup cost impacts unit price) | Economical (Fixed digital ink rate) |
| Unit Price (100+ Pieces) | Very Low (Strong economies of scale) | Moderate to High (Static ink cost per unit) |
| Color Complexity Impact | Cost increases with each additional color | No additional cost for unlimited colors/photos |
| Heavyweight Fabric Performance | Excellent coverage with plastisol/discharge ink | Needs heavy pretreatment & white underbase |
| Turnaround & Setup Speed | 2–5 days screen setup; fast bulk printing | Instant digital setup; 3–15 day sample lead time |
Frequently Asked Questions
When does screen printing become more economical than DTG for heavy t-shirts?
The financial turning point generally occurs between 50 and 100 units for multi-color designs. For orders below 50 pieces, DTG is more budget-friendly because it eliminates screen prep fees. Above 100 pieces, screen printing becomes significantly cheaper as setup costs are distributed over a higher unit volume.
Why does DTG printing cost more on heavyweight cotton tees compared to standard tees?
Heavyweight fabrics have dense yarn structures that absorb more liquid. To ensure artwork remains sharp and opaque, printers must apply thicker layers of chemical pretreatment and a heavy white ink underbase, increasing ink volume and curing time per garment.
What is the best option for detailed photographic graphics on custom apparel?
DTG is ideal for complex photographic imagery or gradient designs on smaller runs. While screen printing can achieve photographic results through simulated process printing, it requires 6 to 10 separate color screens, making it cost-prohibitive unless ordering in large quantities over 300 to 500 units.
Strategic Recommendations & Summary
Determining whether to use screen printing or DTG for heavyweight t-shirts depends on your batch size, artwork color count, and financial goals. Use DTG for design testing, limited collections, or orders under 50 pieces to bypass initial tooling fees. For bulk production over 100 units or simpler color graphics, screen printing offers superior unit cost efficiency and bold ink opacity. Partnering with flexible OEM/ODM manufacturers offering standard shipping terms like FOB Shenzhen or DDP Door-to-Door, alongside fast sampling options, enables smooth scaling. For custom apparel guidance or technical assistance, feel free to contact us at yutianfang88@gmail.com.
About the Manufacturer
Dongguan City Dule Garment Co.,Ltd (DOLUXE) is a premier OEM/ODM streetwear and heavyweight clothing manufacturer founded in 2007 in Humen Town, Dongguan, Guangdong. Spanning two facilities across 15,000 square meters, DOLUXE employs over 200 skilled staff members, producing up to 1.2 million garments annually and releasing over 500 fresh styles each year. Specializing in 480-630 GSM heavyweight hoodies, t-shirts, sweatshirts, and denim, DOLUXE partners with over 200 independent brands across more than 30 countries globally.
REPORT