




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
Understanding Acceptable Tolerance Gaps: From Sliding Window Prototypes to Bulk Extrusion Production
Navigating the Gap Between Prototype Samples and Mass Aluminum Extrusion
Transitioning from an initial golden sample to full-scale manufacturing is a crucial phase in architectural window production. Buyers often wonder what variance is acceptable when scaling up. For high-performance aluminum sliding window profiles, acceptable limits demand profile outer dimension tolerances between ±0.15 mm and ±0.3 mm, wall thickness consistency within ±0.1 mm, and a color variance of ΔE ≤ 1.5. Maintaining exact standards for alloy integrity and seal geometry between prototype runs and mass production lots guarantees optimal weatherproofing and long-term durability.
Key focus areas during high-volume production include:
- Wall Thickness & Precision Geometry: Extruded profiles must adhere to approved golden sample measurements, keeping wall deviation within ±0.1 mm to safeguard load-bearing strength.
- Coating & Color Uniformity: Surface finishes (powder coated or anodized) must follow Qualicoat guidelines, restricting batch color differences to ΔE ≤ 1.5.
- Weather Sealing Integrity: Drainage slots and gasket tracking channels must precisely match prototype specs to mitigate air infiltration and water leaks.
- Broad Application Range: Essential for architectural installations, such as Aluminum Sliding Windows, Aluminium Sliding Doors, and facade curtain wall systems.
Key Technical Tolerance Limits: Sample vs. Bulk Manufacturing
To establish clear quality standards, manufacturers and buyers refer to precise technical tolerance boundaries. Deviations beyond these thresholds can jeopardize frame assembly or compromise structural stability:
| Inspection Parameter | Approved Sample Target | Acceptable Bulk Tolerance Limit | Rejectable Variance Threshold |
|---|---|---|---|
| Profile Wall Thickness | Nominal design thickness (e.g., 1.4 mm - 2.0 mm) | ±0.10 mm | > ±0.15 mm (Compromises structural load) |
| Cross-Section Outer Dimensions | Exact CAD geometry | ±0.15 mm to ±0.30 mm (Depending on section width) | > ±0.50 mm (Causes frame assembly misalignments) |
| Surface Coating Thickness | Powder Coating: 60–80 μm | ≥ 60 μm (Qualicoat standard compliance) | < 50 μm (Leads to early oxidation or chalking) |
| Color Consistency (ΔE) | Baseline Master Sample | ΔE ≤ 1.5 | ΔE > 2.0 (Visible shade variation across panels) |
| Alloy Hardness & Temper | 6063-T5 / ≥ 8 Webster Hardness (HW) | 8 – 12 HW | < 8 HW (Insufficient strength under wind pressure) |
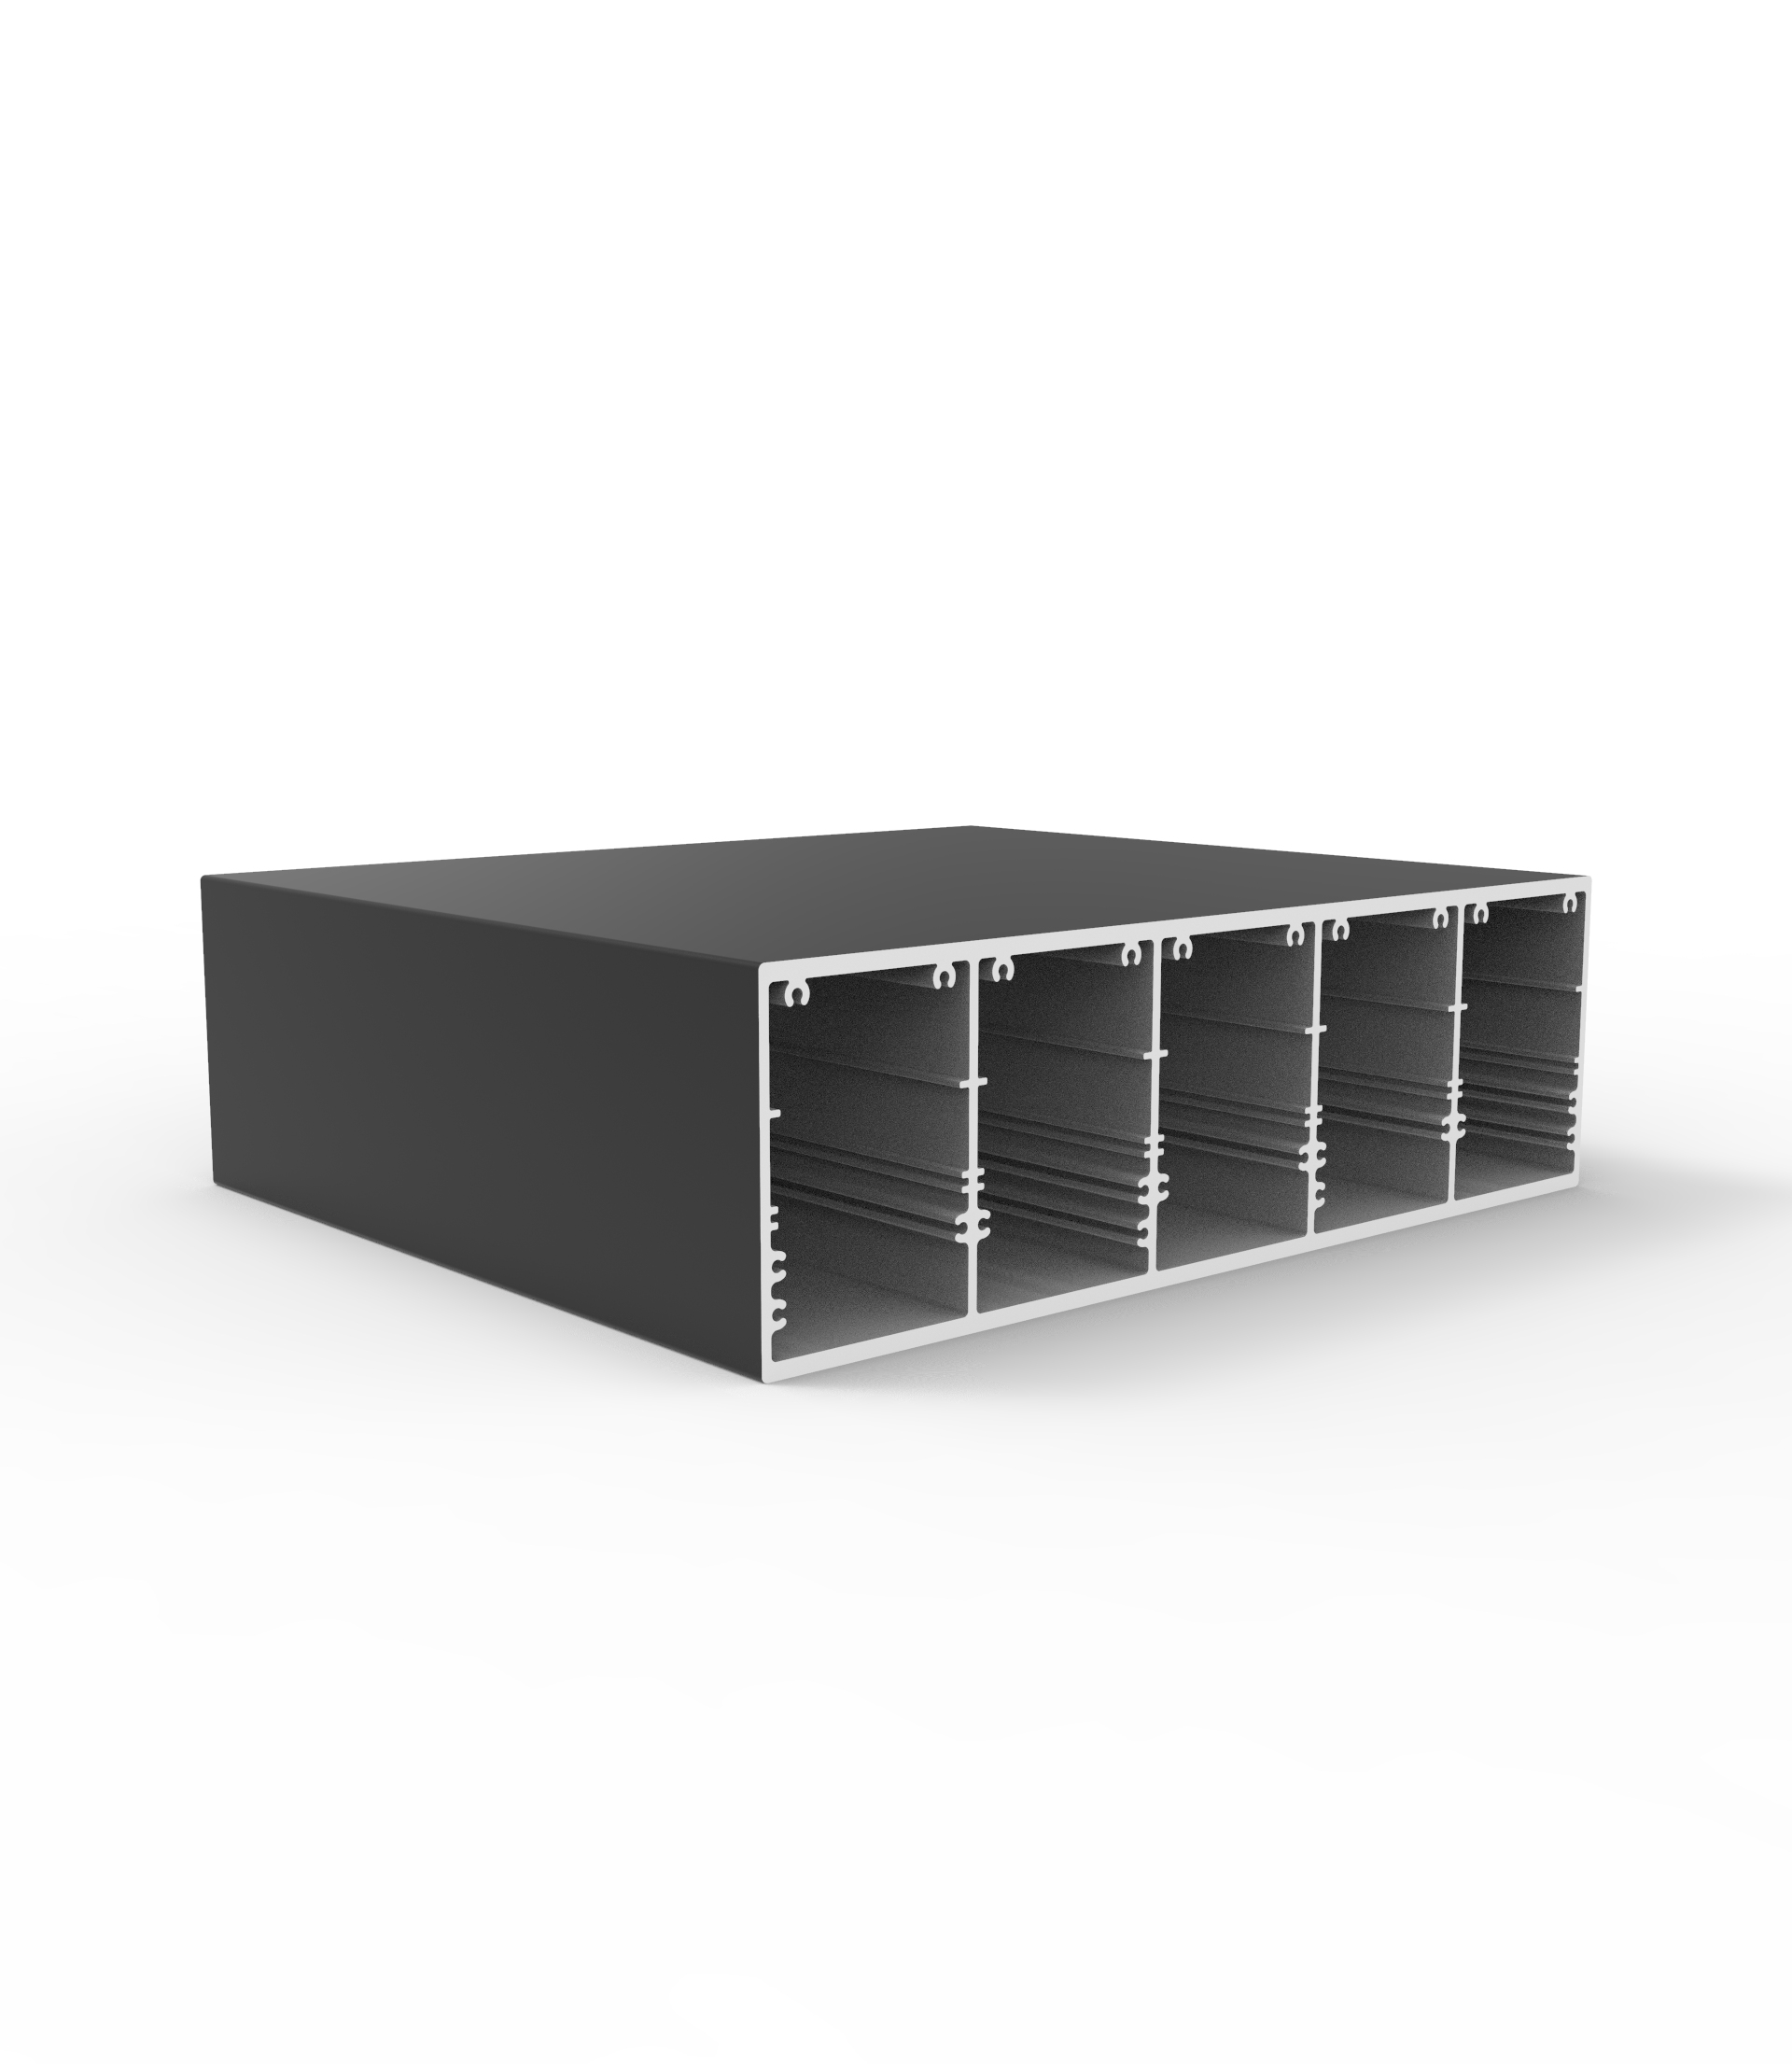
Engineering Principles and Quality Assurance Protocols
Extrusion variance naturally arises due to billet thermal fluctuation, multi-cavity die wear, and aluminum alloy expansion dynamics during continuous runs. Utilizing high-grade virgin 6063-T5 aluminum alloy ensures straightness, structural stiffness, and resistance against warping under volume production.
Strict multi-tiered quality control prevents defective batches from reaching the site. Certified testing facilities under CNAS accreditation (e.g., CNAS L 10434) deploy specialized machinery to measure tensile performance, web thickness, and coating adhesion. Furthermore, international benchmarks like Qualicoat (3419) and SIRIM (PC003807) establish objective boundaries for weatherproofing and surface protection against UV and salt spray exposure. A notable example is The Wan Guo Building Project on Batam Island, where strict profile tolerance management guaranteed exact corner bracket sealing and multi-point lock engagement despite challenging environmental conditions.
Frequently Asked Questions
Q1: What factors cause minor variations between sliding window samples and mass extrusions?
Extrusion die wear over time, billet temperature shifts, and varying extrusion speeds naturally cause minor dimensional differences. Automated quality control mechanisms keep these variances within ±0.15 mm to ±0.3 mm so hardware components fit smoothly.
Q2: What is the permitted variance for surface finish and color in volume orders?
A color variation limit of ΔE ≤ 1.5 is standard, ensuring changes are virtually invisible to the naked eye. Powder-coated and anodized treatments certified under Qualicoat guidelines maintain film thickness and luster equivalent to approved pre-production samples.
Q3: How do manufacturers maintain water-tightness and air-tightness in bulk shipments?
Mass-produced profiles undergo thorough ISO 9001-guided laboratory testing. Sealant grooves and EPDM gasket tracks are continuously measured against master technical drawings to guarantee rated air and water tightness performance.
Conclusion & Best Practices for Architectural Procurement
Preventing quality discrepancies when moving from sliding window samples to bulk orders relies on defining strict tolerance rules, using premium alloy compositions, and implementing end-to-end quality monitoring. Specifying explicit metrics (such as ±0.1 mm for wall thickness) prevents assembly issues on-site. Choosing an integrated supplier mitigates risks, ensuring standard lead times of 15–20 days and minimum order quantities of 3 tons for custom profiles. For technical inquiries or custom order consultations, contact xh@xinhealuminium.com.
About Us
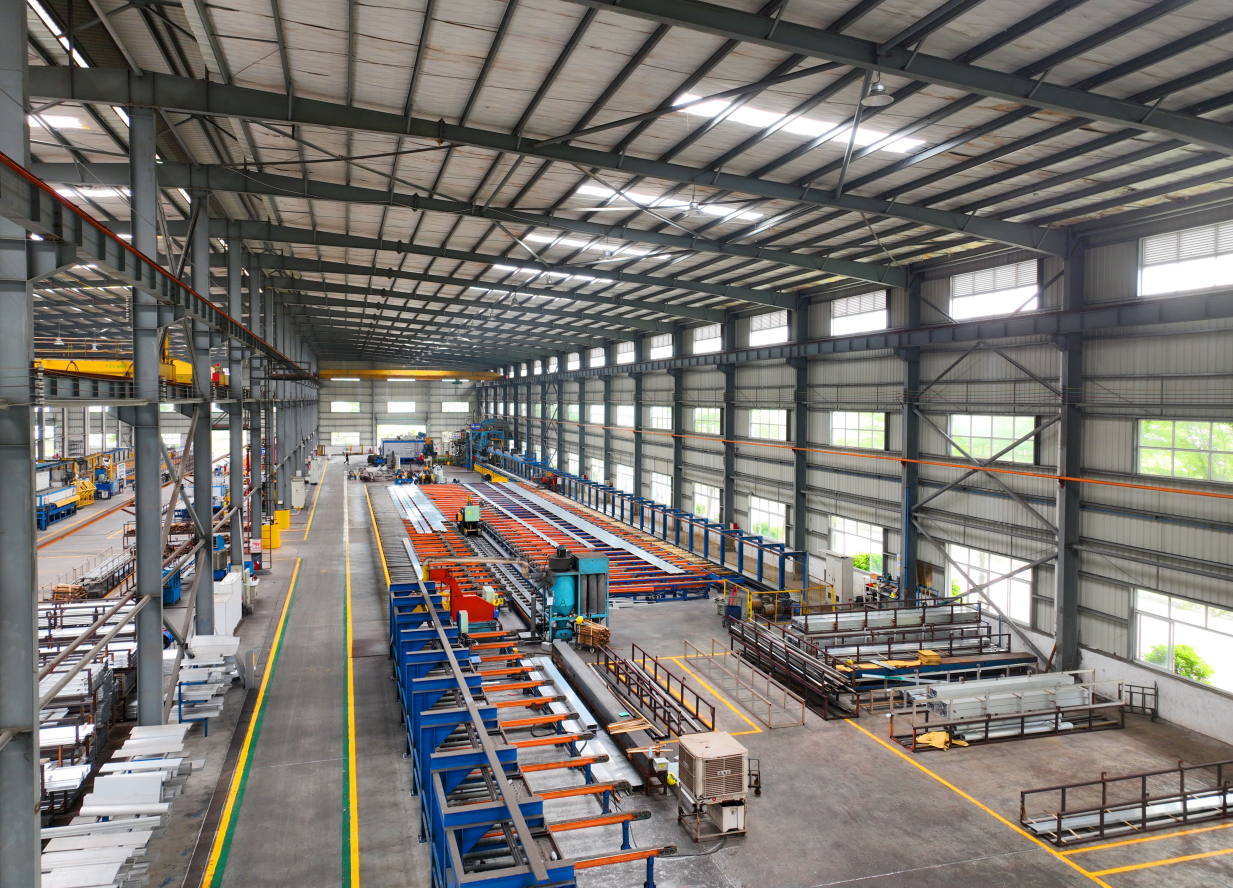
Guangdong Xinhe Aluminium Co., Ltd, founded in 1998, operates an expansive 666,670 sqm manufacturing base with a workforce of 1,200 employees. Housing 60 modern extrusion lines, the company achieves an annual capacity of 200,000 tons across architectural, door, window, and industrial profiles. Supported by a CNAS accredited national laboratory (CNAS L 10434) and certifications including ISO 9001, ISO 14001, Qualicoat, and SIRIM, Xinhe serves client networks throughout Asia, Europe, and Africa.
REPORT